
A label is the last thing applied to a product on the packaging line and the first thing a customer, pharmacist or inspector sees. It carries the product name, strength, batch number, expiry date, barcodes and regulatory information — and in many industries, a single error on that label can trigger a recall.
Yet labelling is often treated as a simple, final step. In reality, labelling problems are among the most common causes of rejects, line stoppages, customer complaints and compliance issues. Wrinkled labels, skewed placement, missing batch codes and mix-ups between products all cost money and damage trust.
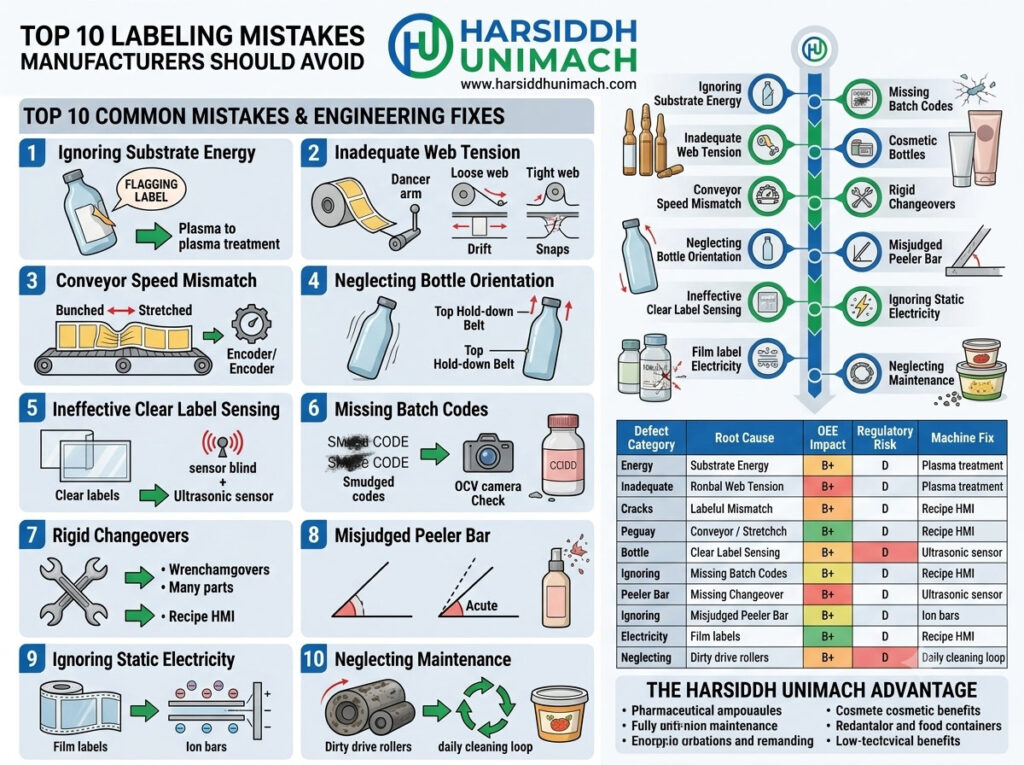
The good news is that most labelling problems have predictable causes. In this guide, we look at the ten most common labelling mistakes manufacturers make — and how to avoid each one.
Why Labelling Mistakes Are So Costly
Labelling errors have consequences far beyond the cost of a wasted label:
- Regulatory risk: incorrect or missing information on pharmaceutical, food or chemical products can lead to recalls and regulatory action.
- Patient and consumer safety: a label mix-up can result in the wrong product or dose being used.
- Product waste: a rejected label often means a rejected container — with the product inside.
- Brand damage: crooked or bubbled labels make even premium products look cheap.
- Lost productivity: frequent stoppages to fix labelling problems reduce line efficiency.
Mistake 1: Choosing the Wrong Labelling Machine for the Container
Containers come in many shapes — round, flat, oval, square, tapered, small vials, fragile ampoules, cartons and tubes — and each needs a specific labelling approach. Using a machine designed for round bottles on flat containers, or forcing a general-purpose labeller to handle tiny ampoules, leads to inconsistent placement, wrinkles and rejects.
How to avoid it: match the machine to the container and label format.
- Round bottles: wrap-around labellers such as the vertical bottle sticker labeling machine. See our labeling machines for round bottles.
- Flat and oval bottles: front-and-back labellers like the Automatic Front and Back Sticker Labeling Machine, or our range of labeling machines for flat bottles.
- Vials: precise wrap-around labellers such as the vertical vial sticker labeller. See all labeling machines for vials.
- Ampoules: horizontal or rotary labellers that handle small, fragile containers gently, such as the Automatic Horizontal Ampoule Sticker Labeling Machine and the rotary ampoule sticker labeling machine.
- Top surfaces of jars, cartons and pouches: the Automatic Top Side Sticker Labeling Machine.
- Full-body decoration and tamper evidence: the Automatic Shrink Sleeve Label Applicator.
To understand how these machines work, read our guide to the bottle labeling machine working principle.
Mistake 2: Ignoring Container Variation and Quality
Even the best labelling machine struggles if containers vary. Differences in diameter, height, wall straightness, surface finish or moulding flash affect how labels are applied. Tapered bottles cause labels to spiral, uneven surfaces cause bubbles, and out-of-round containers lead to overlapping or gaps on wrap-around labels.
How to avoid it:
- Specify container dimensions and tolerances with your container supplier.
- Check incoming containers for dimensional consistency.
- Design labels to suit the container’s actual label panel, avoiding curves, seams and ribs.
- Test new container suppliers on the labelling machine before approving them.
Mistake 3: Using the Wrong Label Material or Adhesive
The label face material and adhesive must suit the product, the container and the conditions the product will face. A paper label may wrinkle in humid storage, a standard adhesive may fail on cold or wet containers, and some adhesives do not bond well to certain plastics. Labels on squeezable bottles need flexible materials that won’t crease or lift.
How to avoid it:
- Tell your label supplier the container material, surface condition, application temperature and storage conditions.
- Choose film labels (such as PP or PE) for moisture, oil or squeeze resistance where needed.
- Select adhesives suited to cold, frozen, wet or curved surfaces.
- Test labels through the full product life cycle, including transport and storage.
Mistake 4: Poor Label Roll Specifications
Labelling machines depend on consistent label rolls. Common problems include the wrong core diameter, incorrect unwind direction, inconsistent gaps between labels, weak release liners that break under tension, and poor die-cutting that leaves labels attached to the matrix. Any of these causes misfeeds, missing labels and stoppages.
How to avoid it:
- Agree a clear label roll specification with your supplier, covering core size, outer diameter, unwind direction, gap, liner type and splice standards.
- Ensure label gaps are compatible with the machine’s label sensor.
- Inspect incoming rolls and reject non-conforming deliveries.
- Store rolls in controlled conditions to prevent curling and adhesive bleed.
Mistake 5: Incorrect Machine Setup and Speed Matching
Many labelling problems come from setup rather than equipment. If the label dispensing speed doesn’t match the container speed, labels stretch, wrinkle or are placed incorrectly. Incorrect peel plate position, wrap-around belt pressure, label sensor calibration or guide settings also cause poor results.
How to avoid it:
- Use servo-driven label dispensing that synchronises automatically with conveyor speed.
- Document setup parameters for every product and container size in machine recipes.
- Calibrate label and product sensors at each changeover.
- Train operators thoroughly on setup and fine adjustment.
For dual-sided labelling, accurate registration is especially important. Our article on how to achieve precise dual-side label placement explains the key setup principles.
Mistake 6: Labelling Wet, Dusty or Cold Containers
Labels need a clean, dry surface to bond properly. Containers that are wet from washing, carry condensation after cold filling, or are dusty or oily from the filling process will cause labels to lift, bubble or fall off — sometimes days later in the warehouse.
How to avoid it:
- Install air knives or drying systems before the labeller where containers may be wet.
- Allow cold-filled containers to stabilise or use adhesives designed for condensation.
- Prevent product drips during filling with drip-free nozzles.
- Keep containers clean and free of dust before labelling.
Mistake 7: Overlooking Coding, Printing and Verification
Batch numbers, manufacturing dates and expiry dates are often printed on labels as they are applied. Smudged, faded, missing or incorrect codes are among the most serious labelling errors, especially for pharmaceuticals. Without verification, these errors can pass unnoticed into the market.
How to avoid it:
- Integrate reliable coding systems with the labelling machine, matched to the label material.
- Use vision systems or OCR/OCV to verify printed text and barcodes.
- Install automatic rejection for unreadable or incorrect codes, with confirmation that rejected containers have actually been removed.
- Verify coding data at the start of every batch and after any change.
As serialization becomes mandatory in more markets, verification becomes even more critical. Learn more in our guide to how serialization is transforming pharmaceutical packaging.
Mistake 8: Weak Line Clearance and Changeover Procedures
Label mix-ups — where labels from one product end up on another — are among the most dangerous labelling errors. They usually happen during changeovers, when leftover labels or rolls from a previous batch remain on or near the line.
How to avoid it:
- Enforce strict line clearance procedures, with documented checks before every new batch.
- Remove and reconcile all labels from the previous batch.
- Use label codes or barcodes that the machine can scan to confirm the correct label is loaded.
- Reconcile label quantities issued, used, rejected and returned for each batch.
- Separate lines physically where products look similar.
Mistake 9: Neglecting Maintenance
Labelling machines contain wear parts that gradually affect performance: rollers, peel plates, brushes, wrap belts, sensors and drive components. As they wear, label placement drifts, wrinkles appear and missing labels become more frequent — often so slowly that operators adjust settings to compensate instead of fixing the root cause.
How to avoid it:
- Follow a preventive maintenance schedule based on running hours.
- Clean adhesive build-up from rollers, guides and peel plates regularly.
- Inspect and replace worn wrap belts, pressure rollers and brushes.
- Keep critical spares in stock.
Our article on high-speed labeling machine maintenance lists the components that need regular inspection.
Mistake 10: Poor Integration with the Rest of the Line
The labeller does not work alone. If upstream machines deliver containers unevenly, labels are applied inconsistently. If capping is incomplete — loose or tilted caps — containers may not sit correctly in the labeller. And if the labeller runs slower than the filler, the line backs up.
How to avoid it:
- Match labeller speed to the filler and capper, with a margin for recovery after stoppages.
- Use accumulation tables or buffer conveyors to smooth container flow.
- Ensure caps are correctly applied by reliable equipment such as a bottle screw and ROPP capping machine.
- Inspect containers before labelling so only good product is labelled, using suitable inspection machines.
- Synchronise controls so the labeller stops and starts with the rest of the line.
Bonus: Skipping Operator Training
Many of the mistakes above trace back to one root cause: operators who have not been fully trained on the machine, the labels and the procedures. Training should cover machine setup, changeovers, label loading, coding verification, line clearance, troubleshooting and basic maintenance. Well-trained operators spot problems early and fix them correctly, rather than covering them up with temporary adjustments.
Quick Troubleshooting Guide
| Symptom | Likely Cause | First Action |
|---|---|---|
| Wrinkled labels | Speed mismatch, tapered container, low wrap pressure | Check servo sync, container dimensions and wrap belt |
| Skewed or misplaced labels | Poor container guidance, incorrect peel plate position | Reset guides and peel plate height |
| Missing labels | Label sensor not calibrated, inconsistent label gaps | Recalibrate sensor, inspect roll specification |
| Bubbles under label | Wet or dusty surface, uneven container | Dry and clean containers, review container quality |
| Labels lifting later | Wrong adhesive, cold or wet application | Review adhesive specification and conditions |
| Faded or smudged codes | Wrong ribbon or ink for label, printer settings | Match coding consumables to label material |
Keeping a simple troubleshooting guide like this beside each line helps operators fix problems quickly and consistently, and recording which symptoms occur most often points to where permanent improvements are needed.
Building a Right-First-Time Labelling Process
Avoiding labelling mistakes comes down to a few principles:
- Specify correctly – the right machine, container, label material and roll specification.
- Set up consistently – documented recipes, calibrated sensors and synchronised speeds.
- Verify automatically – vision inspection for labels and codes, with reliable rejection.
- Control rigorously – line clearance, label reconciliation and change control.
- Maintain proactively – scheduled maintenance and spares.
- Train continuously – skilled operators who understand the whole process.
Applying these principles reduces rejects, prevents mix-ups and keeps your line running smoothly. Explore our full range of labeling machines and the labeling machines on Harsiddh Engineering to find the right solution for your containers.
Frequently Asked Questions
What is the most common labelling mistake? Incorrect machine setup — especially speed mismatch between the label dispenser and the containers — is one of the most frequent causes of wrinkled, skewed or misplaced labels.
Why do labels peel off after application? Usually because containers were wet, cold, dusty or oily during labelling, or because the label adhesive was not suitable for the container material or storage conditions.
How can label mix-ups be prevented? Through strict line clearance, label reconciliation, barcode verification of label rolls and physical separation of similar products.
Why do labels wrinkle on bottles? Wrinkles are often caused by tapered or inconsistent containers, incorrect wrap-around pressure, speed mismatch or unsuitable label materials.
How often should a labelling machine be maintained? Follow the manufacturer’s preventive maintenance schedule, typically based on running hours, with daily cleaning of adhesive build-up and regular inspection of wear parts.
Want a labelling line that gets it right first time? Contact our team or send an inquiry to discuss your requirements.