
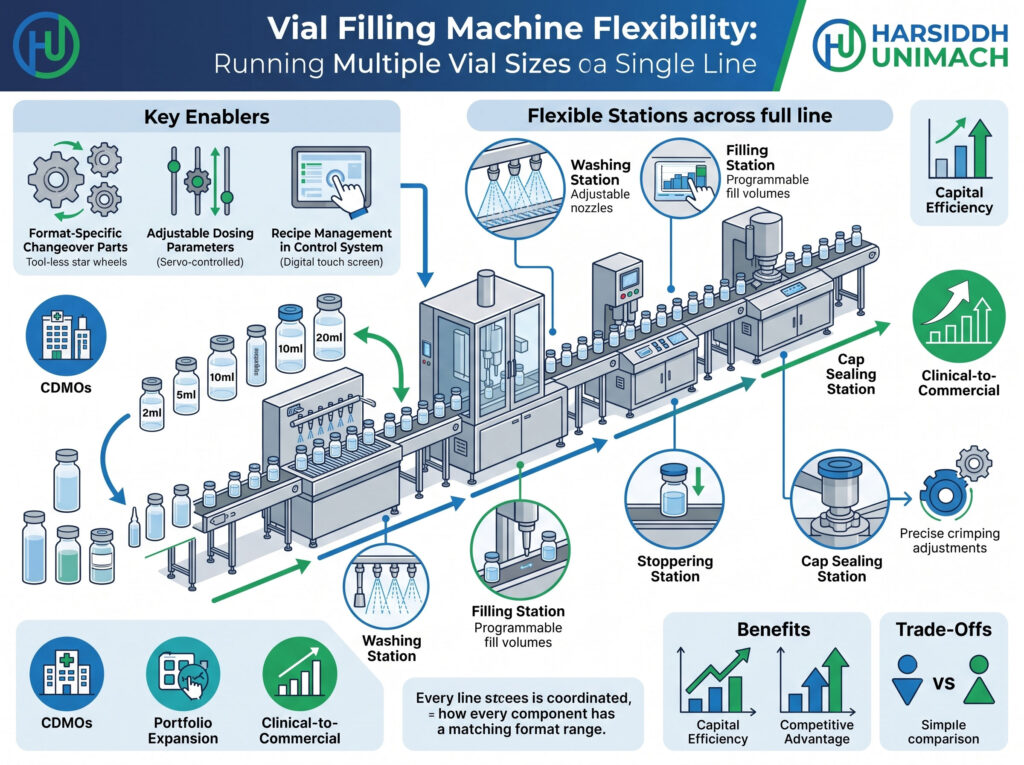
Few injectable manufacturers fill only one product in one vial size. A typical plant may run a 2 ml vial for a paediatric dose in the morning, a 10 ml multi-dose vial in the afternoon and a 20 ml or 30 ml vial for a hospital pack later in the week. Contract manufacturers face even wider variety, because every client brings its own container, stopper and cap.
Buying a separate line for every size is rarely practical. It ties up capital, cleanroom space and validation effort, and most of those lines would sit idle much of the time. The better answer for many plants is a flexible vial filling line: one line designed from the start to run a defined range of vial sizes, with quick, repeatable changeovers between them.
This guide looks at flexibility as a design and specification question. It explains what actually changes between vial formats, how each machine in the line handles different sizes, which design features make multi-format operation easier, how to plan your format range and how qualification works when one line runs many sizes. If you are looking for the step-by-step procedure for the changeover itself, see our companion article on vial filling machine changeover best practices.
Why Flexibility Matters in Vial Filling
Several trends push manufacturers toward multi-format lines:
- Broader product portfolios. Generic and branded companies alike are adding more SKUs, often in smaller batches.
- Contract manufacturing. CMOs and CDMOs must accept whatever container the client specifies, so a line that runs only one size limits the business they can win.
- Smaller batch sizes. Biologics, speciality drugs and clinical supplies are often produced in short runs, so the line changes format more often.
- Space and capital limits. A cleanroom suite is expensive to build and run. One flexible line can replace two or three dedicated ones.
- Market changes. A product may move from a 10 ml multi-dose vial to a 2 ml single-dose vial during its life. A flexible line adapts without new equipment.
Flexibility is not free, however. Every extra format adds change parts, validation work and operator training. The goal is the right amount of flexibility: enough to cover the products you have and expect, but not so much that the line becomes complicated and slow to change.
What Actually Changes Between Vial Sizes
Before specifying a flexible line, it helps to list exactly what differs between your vial formats. Each difference affects one or more machines.
| Vial Feature | Typical Variation | Machines Affected |
|---|---|---|
| Body diameter | Small 2 ml vials to large 50 ml vials | Every machine: star wheels, guides, grippers, conveyors |
| Overall height | Short and tall vials of similar diameter | Washer grippers, needle stroke, stoppering height, capper head height, label position |
| Neck finish | 13 mm, 20 mm or 32 mm crimp necks | Stopper bowl and track, stoppering head, cap feeding, sealing head |
| Fill volume | From fractions of a millilitre to tens of millilitres | Pump size or stroke, dosing settings, fill time |
| Stopper type | Liquid stoppers vs lyophilisation stoppers | Stopper bowl, track, pick-up and insertion settings |
| Cap type | Flip-off, plain aluminium, tear-off | Cap hopper, chute, sealing settings |
| Label size | Varies with vial height and diameter | Labeller roller, guides, label path |
| Glass type | Moulded vs tubular glass | Handling forces, guides, washing grippers |
Two vials that look similar may still need different parts. A 10 ml moulded vial and a 10 ml tubular vial, for example, can differ in diameter and height. That is why the starting point for any flexible line is a container specification for every format, with drawings and tolerances from your glass supplier.
How Each Machine in the Line Handles Multiple Sizes
A complete vial line usually includes a washer, a depyrogenation tunnel, a filling and stoppering machine, a capping machine, an external washer and a labeller. Each handles size changes differently.
Vial Washer
Washers grip, invert and transport vials through rinsing and air-blowing stations. Size changes usually involve:
- grippers or vial holders matched to the body diameter
- infeed star wheel, scroll and guides
- needle height or stroke so the spray reaches the inside of the vial
- outfeed parts that hand vials to the tunnel
An automatic linear vial washer or a linear vial washer handles vials in a straight path, while a rotary vial washing machine uses rotating grippers. Both can run several formats with the right change parts. Check how many parts change per format and whether needle stroke is set mechanically or by recipe.
Depyrogenation Tunnel
The sterilizing tunnel for ampoules and vials is usually the most flexible machine in the line, because vials travel on a wide mesh belt rather than in pockets. Size changes may involve:
- side guides at the infeed and outfeed
- belt speed, which affects time at sterilising temperature
- the validated temperature and time cycle for each format
The key point is validation. A larger vial has more glass mass and heats up differently, so the depyrogenation cycle is normally confirmed for the most demanding format in the range. Your QA team should define this approach.
Filling and Stoppering Machine
The filler sees the most changes, because it handles both container and product:
- Vial handling: infeed scroll or star wheels, guides and centring parts
- Dosing: pump size, piston stroke or peristaltic tube size to suit the fill volume
- Needles: needle size, insertion depth and fill motion (for example, rising with the liquid level for larger vials)
- Stoppering: stopper bowl track, pick-up head and insertion height for each neck size and stopper type
A six head liquid vial filling and stoppering machine or a liquid vial filling machine with rubber stoppering can cover a wide range of fill volumes when the pump and stroke options are specified correctly. An automatic servo based vial filling machine adds the advantage of storing fill and motion settings in recipes, which is explained further below.
Very wide fill ranges sometimes need two pump sizes. A small pump gives good accuracy on small volumes, while a larger pump fills big volumes in a reasonable time. Ask your supplier how fill accuracy changes across the range you plan to run.
Capping Machine
Cap sealing machines crimp aluminium caps over the stopper and vial neck. Size changes typically involve:
- star wheels and guides for the vial body
- cap hopper and chute for the cap diameter
- sealing head or crimping parts for the neck finish
- head height for the vial height
A vial cap sealing machine with 1, 4, 6 or 8 heads or a glass vial capping machine should be specified for every neck size in your range. A change in neck size (for example, from 13 mm to 20 mm) usually means more parts change than a change in body diameter alone.
External Washer and Labeller
After capping, an automatic external vial washing machine removes product residue from the outside of the vial. Size changes are usually limited to guides, star wheels and nozzle positions.
The labeller changes the label roll, label path and guides, and the label position must suit the vial height. A vertical vial sticker labeller can handle a range of diameters. For practical tips on this step, read our guide to handling different vial diameters on a vial sticker labeling machine.
Design Features That Make Multi-Format Operation Easier
When you compare suppliers, these features make the biggest difference to how well a line runs several sizes.
1. Servo Drives and Stored Recipes
On a mechanical machine, settings such as fill stroke, needle depth and timing are adjusted by hand with cams, linkages and scales. On a servo-driven machine, these values can be stored in a recipe for each format and product. The operator selects the recipe on the HMI and the machine sets the motion profile automatically.
Recipes reduce adjustment time, cut the risk of human error and make every changeover repeatable. The engineering differences are covered in detail in our article on how servo-driven vial filling systems outperform mechanical lines. Confirm with your supplier which axes are servo-controlled on the specific model you are considering, as this varies by machine.
2. Tool-Less or Quick-Release Change Parts
Change parts fixed with hand knobs, quick-release pins or locating dowels are much faster to swap than parts held by bolts. They also reduce the risk of dropped tools in the filling zone.
3. Colour Coding and Marking
Marking each change part with the format it belongs to (by colour, engraving or a tag) prevents mix-ups. A 20 ml star wheel and a 30 ml star wheel may look alike, but fitting the wrong one will cause jams or breakage.
4. Repeatable Adjustment Points
Where adjustment cannot be avoided, scales, digital counters or fixed stops let operators return to a known setting rather than adjusting “by eye”. Record the setting for each format in the batch documentation or SOP.
5. Common Parts Across Formats
A well-designed range shares as many parts as possible between formats. For example, two vials with the same neck finish may share the stoppering and capping parts, so only the body-handling parts change. Discuss this with your supplier at the design stage.
6. Easy Access and Cleaning
Change parts that are easy to reach and remove are also easier to clean. On lines with barrier systems, check that changes can be made through glove ports or during planned openings without breaking the cleanroom regime unnecessarily.
Planning Your Format Range
The most important decisions for a flexible line are made before the purchase order. A clear format plan avoids buying parts you never use and missing parts you need later.
Step 1: List Current and Future Products
Write down every product the line will run in the next five years or so, including expected new launches and client projects. For each one, note the vial size, fill volume, stopper, cap, label and expected annual volume.
Step 2: Group by Container Family
Group products that share the same vial, stopper and cap. Each group is one format. You may find that twenty products need only four or five formats.
Step 3: Standardise Where You Can
Before buying change parts for every possible vial, ask whether some products could move to a common container. Standardising on fewer vial sizes, neck finishes and stoppers reduces change parts, spares and validation. This often needs agreement from regulatory, marketing and clients, so start the conversation early.
Step 4: Define the Limits
Every machine has a minimum and maximum vial diameter, height and fill volume. Make sure your smallest and largest formats sit comfortably inside these limits. Formats at the extreme edge of a machine’s range often run slower and less reliably.
Step 5: Check Speed per Format
A line rarely runs every size at the same speed. Large fill volumes need more time at each filling station, and very small vials can be less stable on conveyors. Ask the supplier for the expected output for each format, not just the headline maximum, and plan capacity on realistic numbers.
Step 6: Order Change Parts at the Start
Change parts ordered with the machine can be included in the factory acceptance test and qualification. Parts added later need their own testing and documentation. If you know a format is coming, it is usually easier to include it from the beginning.
Our vial filling line checklist of seven things to evaluate before buying covers the wider buying decision.
Flexible Line vs Dedicated Lines
Flexibility suits some operations better than others. The table below gives a general comparison.
| Factor | One Flexible Line | Several Dedicated Lines |
|---|---|---|
| Capital cost | Lower overall, plus change parts | Higher: one line per size |
| Cleanroom space | Smaller footprint | More space needed |
| Utilisation | High, as the line runs many products | Lower if some products have small volumes |
| Changeover time | Regular changeovers needed | Few or no format changes |
| Output per product | Shared capacity | Full capacity for each product |
| Validation | One line, several formats to qualify | Each line qualified separately |
| Risk | One breakdown stops all products | Other lines keep running |
| Best for | Many products, small to medium batches, CMOs | A few high-volume products |
Many plants use a mix: dedicated high-speed lines for one or two large products and a flexible line for everything else. Our article comparing small vial machines and high-speed vial lines explains how to size each type.
An Illustrative Look at Changeover Time and Capacity
To see why changeover design matters, consider a simple illustrative example. These figures are not performance data for any machine; they only show how the arithmetic works.
Assume a line runs 16 hours a day and changes format once a day.
- If a changeover takes 3 hours, the line has 13 hours of production time, or about 81% of the shift.
- If better design and preparation cut the changeover to 1 hour, the line has 15 hours, or about 94% of the shift.
That 2-hour saving adds roughly 15% more production time each day (15 ÷ 13 ≈ 1.15). On a line that changes format several times a week, quick and repeatable changeovers can be worth as much as a faster filling speed. Use your own shift pattern and changeover frequency to estimate the value for your plant.
Qualification When One Line Runs Many Sizes
A flexible line must be shown to work correctly for every format it runs. This is part of the normal IQ, OQ and PQ programme, but with some extra planning.
- Installation Qualification (IQ): confirms that all change parts for every format were delivered, match the drawings and are correctly identified.
- Operational Qualification (OQ): shows the machine operates correctly across its range. Testing is often done at the smallest and largest formats, plus any format with unusual features.
- Performance Qualification (PQ): shows the line consistently produces acceptable product under real conditions for the formats in use.
Some companies use a bracketing approach, testing the extreme formats on the basis that formats in between will behave similarly. Whether bracketing is acceptable, and which formats need full testing, is a decision for your QA and regulatory teams based on your risk assessment and the applicable guidelines. Fill accuracy, stopper placement, cap seal quality and container integrity are typical points to confirm for each format.
Changeovers themselves should be covered by SOPs, line clearance checks and documentation, so that every format change is controlled and traceable. For more detail on the qualification process, see our guide to automatic vial filling equipment validation and IQ, OQ and PQ.
Managing Change Parts Over Time
Change parts are valuable equipment and need proper management:
- Storage: keep parts in labelled racks or trolleys, one per format, close to the line but outside the critical zone where your procedures require.
- Cleaning: clean and, where required, sterilise parts before use according to your validated procedures.
- Inspection: check for wear, chips and damage before fitting. Worn star wheel pockets or guides can cause vial breakage.
- Records: track which parts were used for each batch and record maintenance and replacement.
- Spares: keep spare wear parts for the formats you run most often, such as gripper pads or pump seals.
A dedicated changeover trolley for each format, with every part and tool in a set position, makes it easy to see if anything is missing before the change starts.
Common Mistakes to Avoid
- Buying the machine first and thinking about formats later. Missing formats can be expensive and slow to add after installation.
- Planning capacity on headline speed. Large or unusual formats may run much slower.
- Too many formats. Each extra size adds parts, training and validation. Standardise where possible.
- Ignoring the rest of the line. A flexible filler is of little use if the washer, tunnel, capper or labeller cannot run the same sizes.
- Poor part identification. Unmarked parts lead to mix-ups and jams.
- No standard procedure. Without SOPs and setting records, every changeover depends on one experienced operator.
Is a Compact Line a Good Option?
For many plants, an integrated line is the most practical way to achieve flexibility. An automatic liquid vial filling line (compact line) brings washing, depyrogenation, filling, stoppering and capping together with matched speeds and coordinated change parts. Because the machines are designed to work together, the format range is defined for the whole line rather than machine by machine, which simplifies planning and qualification.
Frequently Asked Questions
How many vial sizes can one line run? There is no fixed number. It depends on the machine’s diameter, height and volume limits and on the change parts purchased. Many lines run several formats within a defined range. Share your vial list with the supplier for a firm answer.
Can one line run both 13 mm and 20 mm neck vials? Often yes, with the correct stoppering and capping parts for each neck size. Confirm with the supplier for the specific model.
Do I need different pumps for different fill volumes? Sometimes. A wide range of fill volumes may need two pump or tube sizes to keep accuracy and speed acceptable across the range.
Does every format need full validation? Every format must be shown to work correctly. Whether testing can be bracketed is a QA and regulatory decision based on your risk assessment.
Can change parts be added after installation? Usually yes, but they need to be manufactured to match the machine and then qualified. It is simpler to include known formats in the original order.
Is a servo machine essential for flexibility? Not essential, but servo drives with stored recipes make changeovers faster and more repeatable, especially when formats change often.
Talk to Harsiddh About a Multi-Format Vial Line
Harsiddh Unimach designs and manufactures vial washers, depyrogenation tunnels, filling and stoppering machines, cap sealing machines, external washers and labellers that can be specified to run a defined range of vial sizes. Our team can review your vial drawings, fill volumes, stoppers and caps and recommend the change parts and line configuration that fit your products today and in the future.
Share your format list with us through our contact page or send an enquiry through our inquiry form, and we will help you plan a vial filling line that is flexible, efficient and ready for validation.