
A filling machine’s brochure usually shows one big number: its maximum speed. But that figure, measured under ideal conditions with an easy product, rarely matches what the machine will deliver on your line with your product, containers and shift pattern. Buying on headline speed alone is one of the most common reasons pharmaceutical lines end up either short of capacity or carrying expensive, under-used equipment.
A better approach is to work out the speed you actually need, then understand what determines the speed a machine can actually achieve. This technical guide shows how. It covers calculating required output from demand, understanding cycle time and fill time, choosing the number of heads, intermittent versus continuous motion, the effect of accuracy on speed, line balance and the impact of changeovers.
All numerical examples in this guide are illustrative only, designed to show how the calculations work. They are not performance data for any particular machine. Use your own figures and confirm machine performance with your supplier.
Step 1: Calculate the Speed You Actually Need
Start with demand, not with the machine. The required machine speed depends on how many units you need, how much time is available and how efficiently the line runs.
The Basic Formula
Required rated speed (units per minute) = Annual demand ÷ (Production days × Hours per day × 60 × Expected line efficiency)
Line efficiency accounts for everything that stops or slows the line: changeovers, cleaning, breakdowns, minor stops, start-up and rejects. Many manufacturers track this as Overall Equipment Effectiveness (OEE).
Illustrative Example
- Annual demand: 12 million units
- Production days: 250 per year
- Shifts: two 8-hour shifts (16 hours per day)
- Expected line efficiency: 70%
Required rated speed = 12,000,000 ÷ (250 × 16 × 60 × 0.70) ≈ 71 units per minute
If you had assumed 100% efficiency, you would calculate 50 units per minute and buy a machine that cannot meet demand. The efficiency assumption matters a great deal, so base it on your own experience or a cautious estimate.
Allow for Growth
Add a margin for expected growth in demand over the machine’s life. A machine sized exactly for today’s demand may become a bottleneck in a few years.
Step 2: Understand Cycle Time and Fill Time
Once you know the speed you need, look at what determines a machine’s achievable speed. For most pharmaceutical fillers, speed depends on cycle time and number of heads.
What Makes Up a Cycle
On an intermittent-motion machine (where containers stop under the filling heads), one cycle typically includes:
- Indexing: moving containers into position
- Nozzle or needle movement: lowering into the container
- Filling: dispensing the product
- Retraction: raising the nozzle or needle, often with drip control
- Closing (if integrated): stoppering or other operations, often in parallel at another station
Fill Time Depends on Volume and Product
Fill time is often the largest part of the cycle. It depends on:
- Fill volume: larger volumes take longer
- Viscosity: thick products flow slowly
- Foaming: foaming products must be filled more slowly, sometimes bottom-up
- Container opening: narrow necks limit flow
- Product sensitivity: shear-sensitive products such as some biologics may need gentle filling
As a simple illustration, if a product can be dispensed at 5 ml per second without splashing or foaming, a 10 ml fill takes about 2 seconds.
Calculating Machine Speed
Machine speed (units per minute) = Number of heads × 60 ÷ Cycle time (seconds)
Illustrative example: a six-head machine with a 2.5-second fill and a 1.5-second index and nozzle movement has a 4-second cycle.
Speed = 6 × 60 ÷ 4 = 90 units per minute
Now consider a more viscous product on the same machine, needing a 5-second fill. The cycle becomes 6.5 seconds.
Speed = 6 × 60 ÷ 6.5 ≈ 55 units per minute
The same machine runs at very different speeds depending on the product. That is why it is essential to ask suppliers for the expected speed for your product, fill volume and container, not just the maximum.
Step 3: Choose the Right Number of Heads
Adding heads is the most direct way to increase output, because more containers are filled in each cycle.
Illustrative example: with a 4-second cycle, moving from six heads to eight heads increases speed from 90 to 120 units per minute.
However, more heads also bring:
- higher machine cost
- more product-contact parts to clean, sterilise and change over
- more pumps or dosing units to calibrate and maintain
- a larger footprint
- more product held in the system, which matters for high-value products
| Number of Heads | Typical Application |
|---|---|
| Single head | Lab, R&D, pilot and very small batches |
| Two to four heads | Small to medium production |
| Six to eight heads | Medium to high production |
| More heads or multiple machines | High-volume production |
For vials, a six head liquid vial filling and stoppering machine or a liquid vial filling machine with rubber stoppering suits many production needs. For ampoules, options range from a single head ampoule filling and sealing machine for small batches to an eight head ampoule filling and sealing machine or an automatic high-speed vertical ampoule filling and sealing machine for high volumes.
Our comparison of small vial machines and high-speed vial lines explores this capacity decision in more depth.
Step 4: Intermittent vs Continuous Motion
Filling machines move containers in one of two basic ways.
Intermittent Motion
Containers stop under the heads for filling, then move on. This is common in linear machines and many vial, ampoule and bottle fillers.
- Advantages: precise positioning, simpler design, suitable for a wide range of products and volumes
- Limitations: speed limited by start-stop motion and fill time
Continuous Motion
Containers move continuously while nozzles travel with them, typically on a rotary machine.
- Advantages: higher speeds, smoother container handling
- Limitations: more complex, often less flexible for frequent format changes
For most small and medium pharmaceutical operations, intermittent-motion machines offer the best balance of speed, accuracy and flexibility. Continuous-motion machines suit high-volume products with few changeovers.
Step 5: Match the Dosing Technology to Speed and Accuracy
The dosing system affects both how fast and how accurately you can fill.
| Dosing Technology | Speed Considerations | Accuracy Considerations | Typical Use |
|---|---|---|---|
| Gravity | Good for thin liquids; slows with viscosity | Depends on level and time control | Oral liquids |
| Piston | Handles a wide viscosity range | Very good, volume set by stroke | Injectables, syrups, creams |
| Peristaltic | Moderate; tubing size limits flow | Good, especially at small volumes | Sterile liquids, high-value products |
| Auger | Depends on powder flow | Depends on powder density consistency | Powders |
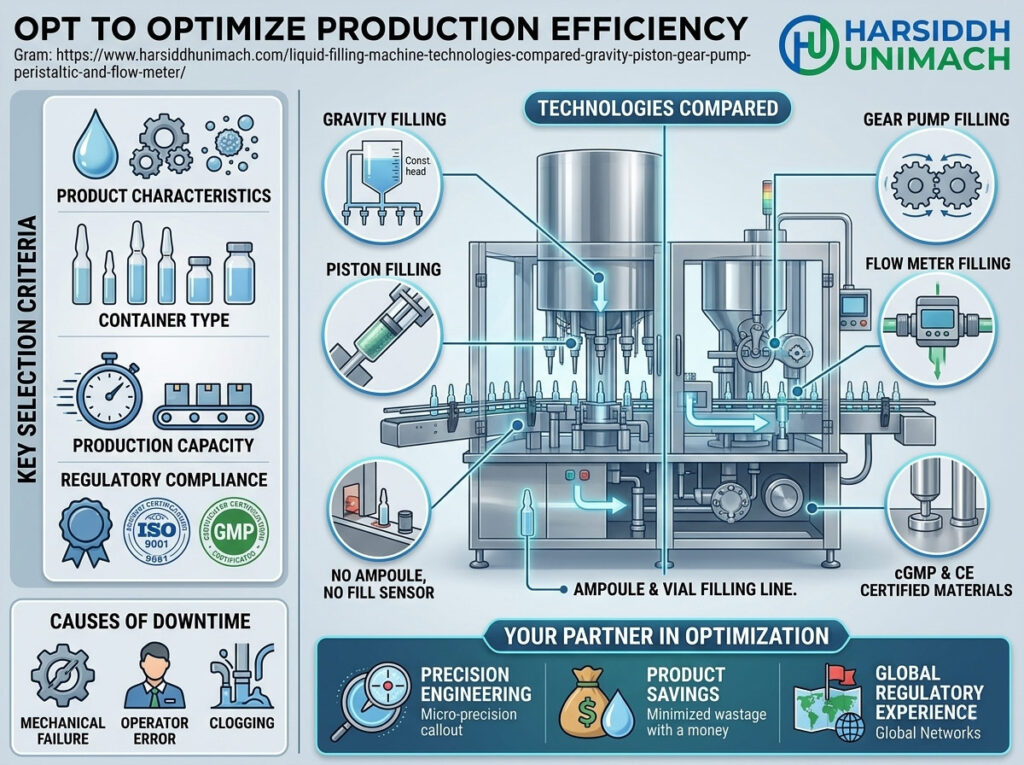
A gravity based liquid filling machine suits thin oral liquids, while a peristaltic based liquid filling machine suits applications needing disposable product paths. For powders, an automatic rotary dry syrup powder filling machine or an auger type powder filling machine are common choices. For creams and ointments in tubes, an automatic double head tube filling machine offers higher output than a single-head machine.
Our technical comparison of liquid filling machine technologies covers each option in more detail.
Step 6: Understand the Speed–Accuracy Trade-Off
Filling faster is not always better. Higher fill speeds can cause:
- splashing and foaming
- product on the container neck, affecting stoppering or sealing
- greater variation in fill volume
- drips at the end of the fill
Many machines use two-stage filling: a fast main fill followed by a slow top-up, or a fill profile that slows near the end. Servo-driven dosing makes this easy to program and repeat. Our article on how servo-driven vial filling systems outperform mechanical lines explains how servo motion profiles improve both speed and accuracy.
Remember that poor accuracy costs efficiency too. Rejected containers and higher overfill targets both reduce effective output.
Step 7: Balance the Line Around the Filler
A filler only achieves its potential if the rest of the line keeps up. Machines upstream and downstream should typically be capable of running somewhat faster than the filler, with buffers to absorb short stops.
- Upstream: a bottle unscrambler, washer or depyrogenation tunnel must feed containers steadily.
- Downstream: cappers, such as a linear capping machine, sealers and labellers must clear containers quickly.
An integrated system, such as an automatic liquid vial filling line, is designed with matched speeds and controlled transfers from the start.
For more on line balancing, see our guide to optimising your pharmaceutical packaging line around the filling machine.
Step 8: Account for Changeovers and Cleaning
On lines that run many products, changeovers can consume more production time than slow running. Include them in your capacity calculation.
Illustrative example: a line runs 16 hours a day. If it changes product once a day and each changeover takes 2 hours, only 14 hours remain for production, before any other losses.
Ways to reduce changeover impact:
- quick-release product-contact parts
- disposable product paths
- stored recipes on servo machines
- format parts prepared in advance
- campaign planning to group similar products
When comparing machines, ask suppliers for typical changeover and cleaning times for your products, not just filling speed.
Step 9: Plan for Downtime and Minor Stops
Even with a perfect design, real lines lose time to:
- container jams and tipping
- empty hoppers or stopper bowls
- sensor faults
- nozzle blockages or drips
- breakdowns
These losses are part of the efficiency figure in Step 1. A machine that is robust, easy to clear and well supported with spare parts will deliver more real output than a nominally faster but less reliable one. Our article on understanding common causes of downtime in pharmaceutical filling lines explains how to reduce these losses.
Putting It All Together: A Technical Selection Worksheet
Use this worksheet when evaluating filling machines:
| Item | Your Value |
|---|---|
| Annual demand (units), now and in 5 years | |
| Production days per year | |
| Hours per day | |
| Expected line efficiency (%) | |
| Required rated speed (units/min) | |
| Product viscosity and behaviour | |
| Fill volume range | |
| Container type and sizes | |
| Required fill accuracy | |
| Expected fill time per container (from trials or supplier) | |
| Cycle time (s) | |
| Number of heads needed | |
| Changeovers per week and time per changeover | |
| Upstream and downstream machine speeds |
Share this worksheet with suppliers so they can propose a machine based on your real requirements.
Common Technical Mistakes
- Using headline speed instead of speed for your product and volume.
- Assuming 100% efficiency in capacity calculations.
- Ignoring fill time for viscous or foaming products.
- Choosing too many heads, adding cost and changeover time without real benefit.
- Pushing fill speed at the expense of accuracy and neck cleanliness.
- Overlooking changeovers in capacity planning.
- Forgetting line balance, so the filler waits for slower machines.
Frequently Asked Questions
How do I calculate how many filling heads I need? Work out the required speed from demand and efficiency, estimate cycle time for your product and volume, then use: heads = required speed × cycle time ÷ 60. Round up and allow for growth.
Why does my machine run slower than its rated speed? Rated speeds are often measured with easy products and small volumes. Viscous products, large volumes, foaming and line stops all reduce real speed.
Is a rotary filler always faster than a linear one? Rotary continuous-motion machines can reach higher speeds, but linear intermittent machines are often more flexible and suit many pharmaceutical applications.
What line efficiency should I assume? Use data from your own lines if available. If not, use a cautious estimate and discuss it with your supplier.
Should I test my product before buying? Yes, wherever possible. A trial gives real fill times and accuracy for your product.
Get a Technically Sized Filling Solution From Harsiddh
Harsiddh Unimach manufactures filling machines for liquids, powders, creams, injectables and more, in single and multi-head configurations, along with the unscramblers, washers, cappers and labellers that complete the line. Share your demand, product and container details, and our engineers will help you size the right machine for your production goals.
Contact us through our contact page or send your requirements through our inquiry form.