
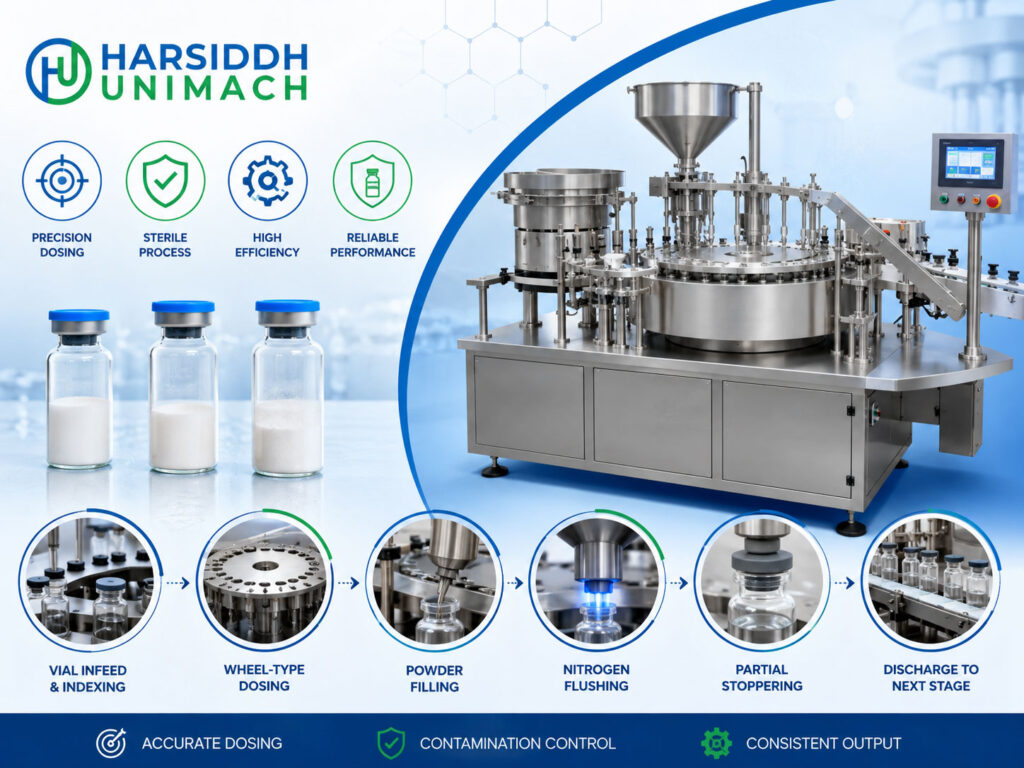
Many important injectable medicines cannot be supplied as ready-to-use solutions. Some antibiotics, such as certain cephalosporins and penicillins, along with other molecules, are not stable for long in water. These products are supplied as sterile dry powder in glass vials, and the powder is reconstituted with a diluent just before injection.
Filling these vials is one of the most demanding tasks in pharmaceutical manufacturing. Each vial has to receive an accurate dose of a fine, often cohesive powder, under aseptic conditions, and then be closed with a rubber stopper before anything can contaminate it. The vial powder filling machine is designed for exactly this job.
In this article, we walk through the machine from end to end: how vials enter, how the powder wheel measures and transfers each dose, how stoppers are placed, how fill weight is controlled and how the machine fits into a complete sterile powder line. For the underlying dosing principles across all powder fillers, read our article on the powder filling machine working principle.
Where the Machine Sits in a Sterile Powder Line
A typical dry powder injection line runs in this order:
- Vial washing, for example on a rotary vial washing machine
- Depyrogenation in a sterilizing tunnel for ampoules and vials
- Powder filling and rubber stoppering (the subject of this article)
- Aluminium cap sealing
- External vial washing, to remove any powder traces from the outside of sealed vials
- Visual inspection
- Labelling and packing
Vials leave the tunnel sterile, depyrogenated and cooled, and enter the filling machine inside the aseptic area, usually under unidirectional airflow.
Main Components of a Vial Powder Filling Machine
- Infeed turntable – receives vials from the tunnel and feeds them into a single line.
- Vial transport system – a star wheel or indexing wheel that moves each vial to the filling and stoppering stations in exact step.
- Powder hopper – holds the sterile powder above the dosing wheel.
- Agitator or stirrer – keeps the powder moving and prevents bridging.
- Powder wheel (dosing wheel) – a precision wheel with dosing ports around its edge.
- Dosing port pistons or plugs – adjust the depth, and therefore the volume, of each port.
- Vacuum system – draws powder into each port and holds it there.
- Blow-off system – sterile, filtered compressed air or nitrogen that ejects the dose into the vial.
- Stopper bowl and chute – a vibratory bowl that orients rubber stoppers and feeds them to the stoppering station.
- Stoppering head – picks up a stopper and presses it into the vial neck.
- Outfeed turntable – collects stoppered vials for transfer to the sealing machine.
- Control panel and sensors – speed control, “no vial, no fill”, “no vial, no stopper”, stopper presence and safety interlocks.
Step-by-Step Working Principle
Step 1: Vial infeed
Sterile vials arrive on the infeed turntable from the tunnel. The turntable gently guides them into a single file. A worm or star wheel then separates the vials and indexes each one into a pocket on the main transport wheel. From this point, each vial travels in exact synchronisation with the powder wheel.
Step 2: Powder presentation in the hopper
The hopper sits directly above the powder wheel. An agitator turns slowly inside the hopper, keeping the powder loose and evenly presented to the wheel. The hopper level is kept within a set range, either by the operator or by an automatic top-up system, because a changing powder column changes how densely powder enters the ports.
Step 3: Port filling under vacuum
The powder wheel rotates. As each dosing port passes beneath the hopper, vacuum is applied behind a fine filter at the base of the port. The vacuum draws powder into the port and packs it to a consistent density.
The port’s volume is set by the position of a small piston or plug inside it. Moving the piston deeper increases the volume and therefore the fill weight; moving it up reduces it.
Step 4: Levelling
As the port leaves the hopper, a scraper or doctor blade wipes the powder level with the surface of the wheel. Excess powder stays in the hopper. Each port now holds a defined, compacted plug of powder.
Step 5: Transfer to the vial
The vacuum continues to hold the powder plug in the port as the wheel rotates it towards the bottom position. At this point the port is directly above the open vial, which is positioned precisely beneath it by the transport wheel.
Step 6: Blow-off
The vacuum is cut off and a short, controlled pulse of sterile filtered air or nitrogen blows the powder plug out of the port and into the vial. Timing and pressure are set so the full dose is released cleanly without scattering powder onto the vial neck or the machine.
Nitrogen is used for oxygen-sensitive products, helping to protect the powder in the vial headspace.
Step 7: Port cleaning and refill
The empty port continues round. Some designs apply a brief cleaning pulse to clear the filter before the port returns under the hopper and the cycle repeats.
Step 8: Rubber stopper feeding
Meanwhile, sterilised rubber stoppers are loaded into a vibratory bowl. The bowl orients the stoppers, usually with the plug pointing down, and feeds them along a track to the stoppering station. A sensor checks that stoppers are present.
Step 9: Stoppering
The filled vial moves to the stoppering station. The stoppering head picks up a stopper and presses it into the vial neck to the correct depth. Fully inserting the stopper is common for dry powder vials, since the product is not freeze-dried in this process. The stopper protects the sterile powder immediately after filling.
The quality of stopper placement has a direct effect on closure integrity. Our article on vial filling machine stoppering: how stopper placement affects container closure quality explains this in more detail.
Step 10: Outfeed
Stoppered vials leave the transport wheel and collect on the outfeed turntable. From here they move to the cap sealing machine, where an aluminium seal is crimped over the stopper, for example on a vial cap sealing machine (1, 4, 6, 8 head). For the sealing process, read our vial cap sealing machine working principle.
Machine Designs
Single wheel, volumetric
One powder wheel doses one vial at a time. This design is well suited to small and medium batch sizes and to plants that run many products. See the Automatic Injectable Vial Dry Powder Filling and Stoppering Machine (Single Wheel Head, Volumetric) and the single wheel injectable dry powder vial filling with rubber stoppering machine.
Double wheel
Two powder wheels work together. They can share the fill to increase output, or dose two different powders into the same vial for combination products. See the Automatic Injectable Vial Dry Powder Filling and Stoppering Machine (Double Wheel Head) and the double wheel injectable dry powder filling machine with vial rubber stoppering.
Servo-based
Servo motors drive the powder wheel and vial transport, giving precise synchronisation, smooth motion and stored recipes for each product and vial size. Servo machines are quicker to set up and very repeatable. See the Automatic Injectable Vial Dry Powder Filling and Stoppering Machine (Servo Based).
| Feature | Single Wheel | Double Wheel | Servo-Based |
|---|---|---|---|
| Dosing wheels | One | Two | One or two |
| Output | Small to medium | Higher | Medium to high |
| Combination fills | No | Yes | Depends on configuration |
| Changeover | Mechanical adjustment | Mechanical adjustment | Recipe-based, faster |
| Repeatability | Good | Good | Very good |
Explore all powder filling machines and the injectable powder filling machines range.
How Fill Weight Is Controlled
Because the powder wheel measures volume, fill weight depends on how densely powder packs into each port. Weight control therefore relies on several settings working together:
| Control | What It Does |
|---|---|
| Port piston position | Sets the volume of each port, the main fill adjustment |
| Vacuum level | Determines how firmly powder is packed into the port |
| Agitator speed | Keeps powder presentation even, avoiding bridging or over-aeration |
| Hopper level | Keeps the pressure of the powder column on the ports consistent |
| Blow-off pressure and timing | Makes sure each port empties completely |
| Wheel speed | Gives each port enough time under the hopper to fill |
In-process weight checks
Operators remove sample vials at defined intervals, weigh them (usually as gross weight minus the average tare of empty vials and stoppers, or by weighing individual vials before and after filling), and adjust the port setting if the trend moves towards a limit. The sampling frequency and limits are defined in the batch documentation.
Why weight drifts
The most common reasons are a falling hopper level, a change in powder density between lots, rising humidity or partially blocked port filters. Good practice is to check all of these before adjusting the port volume.
Aseptic Design Features
Because the product cannot be terminally sterilised in most cases, the filling machine is designed to protect the open vial:
- Unidirectional airflow over the filling and stoppering zones
- Restricted access barriers or isolators in many modern installations
- Contact parts such as hopper, wheel, stopper bowl and chutes that are easy to remove for cleaning and sterilisation
- Smooth, polished surfaces that do not trap powder
- Filtered air or nitrogen for blow-off
- Interlocks such as “no vial, no fill” and “no vial, no stopper” to prevent powder and stopper waste
- Minimal open time between filling and stoppering
Always confirm the specific design requirements against your own quality procedures and the current applicable regulatory guidelines.
Dust Control
Powder dust in an aseptic area is a concern for both product cross-contamination and operator exposure. Machines control dust by enclosing the dosing area, fitting extraction points near the wheel, setting blow-off pressure carefully and keeping the gap between the port and the vial mouth small. After sealing, vials are often cleaned on an automatic external vial washing machine to remove any residual powder from the outside.
Inspection and Labelling
After sealing, each vial is inspected for fill presence, foreign particles, damaged glass and sealing defects. See the Automatic Visual Vial Dry Powder Inspection Machine and the visual vial dry powder inspection machine. Vials are then labelled, for example on a vial sticker labeling machine.
Changeover Between Vial Sizes and Products
A changeover typically involves:
- Changing the star wheels and guides for the new vial size
- Changing the stopper bowl tooling, track and stoppering head parts for the new stopper
- Setting the port volume for the new fill weight, or fitting a wheel with a different port size
- Adjusting the height of the powder wheel and stoppering station
- Cleaning and sterilising all product contact parts between products
- Running trial vials and confirming fill weight before releasing the batch
Recipe storage on servo machines and clearly labelled change parts help reduce changeover time.
Troubleshooting Common Problems
| Problem | Likely Cause | Corrective Action |
|---|---|---|
| Low fill weight | Low vacuum, blocked filters, low hopper level | Check vacuum, clean or replace filters, top up hopper |
| High fill weight | Port set too deep, powder more dense | Reduce port volume, check powder lot |
| Variation between ports | Worn or mismatched port pistons, uneven filter condition | Inspect and match port parts |
| Powder on vial neck | Blow-off pressure too high, poor alignment | Reduce pressure, align vial under port |
| Powder bridging in hopper | Agitator speed too low, humid powder | Adjust agitator, control room humidity |
| Missing stoppers | Stopper bowl empty or track jam | Refill bowl, clear and adjust track |
| Stoppers raised or tilted | Wrong head height, stopper or vial dimensions out of tolerance | Adjust head, check components |
| Vials falling or jamming | Wrong change parts, worn star wheels | Fit correct parts, replace worn items |
Maintenance Tips
- Inspect and replace port filters on schedule; partially blocked filters are a common cause of weight drift.
- Check port pistons and wheel surfaces for wear and scratches.
- Verify the vacuum pump and blow-off filters regularly.
- Keep the stopper bowl and track clean and correctly set.
- Lubricate drive components outside the aseptic zone as per schedule.
- Record and trend fill weights so slow changes are noticed early.
Related Reading
To compare vacuum wheel filling with other powder dosing methods, read types of powder filling machines: auger, gravity and vacuum explained. It shows where auger and gravity fillers fit, for example for dry syrup bottles, and why vacuum filling is so widely used for sterile powder in vials.
Frequently Asked Questions
What is the working principle of a vial powder filling machine? A powder wheel with precision ports draws powder in under vacuum, levels each dose, and then blows it into the vial with sterile air or nitrogen. The vial is then closed with a rubber stopper.
How is fill weight adjusted? Mainly by changing the depth of the piston in each dosing port, supported by stable vacuum, agitation and hopper level.
What is the difference between single and double wheel machines? A single wheel machine uses one powder wheel. A double wheel machine uses two, for higher output or for dosing two powders into one vial.
Why is nitrogen used for blow-off? For oxygen-sensitive products, nitrogen protects the powder and the vial headspace from oxygen.
What happens to vials after powder filling? They are cap sealed with aluminium seals, externally washed, inspected and labelled.
Planning a dry powder injection line? Contact our team or send an inquiry with your vial sizes, fill weights and powder details.