
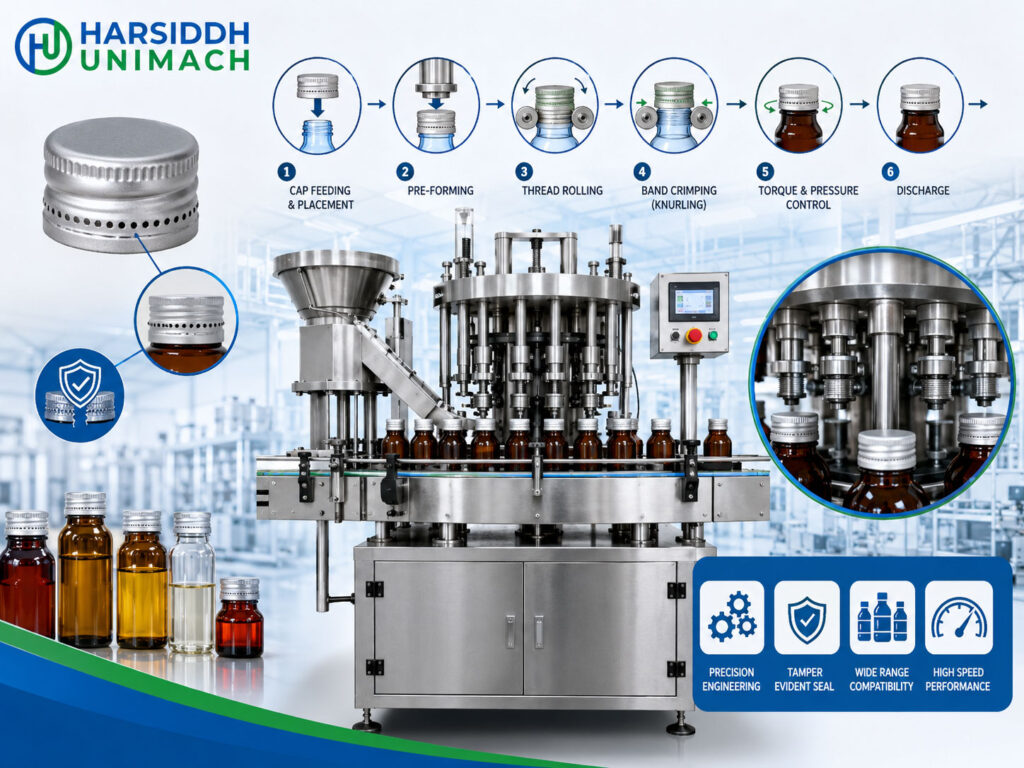
Pick up a bottle of cough syrup, tonic or liquor and twist the cap. You will feel a slight resistance, then a click as a band at the bottom of the cap breaks away and stays on the bottle neck. That is a ROPP cap — roll-on pilfer-proof — and it tells you the bottle has not been opened before.
ROPP caps are popular in pharmaceuticals, beverages and food because they combine a reliable seal with clear tamper evidence. But unlike ordinary screw caps, ROPP caps arrive at the factory without threads. The threads are formed on the cap during capping, by rollers that press the soft aluminium into the bottle’s threads. This makes the ROPP capping machine quite different from a standard screw capper.
In this article, we explain how a bottle ROPP capping machine works, from cap and bottle design to the action of threading and pilfer-proof rollers, the types of machines available, the settings that matter and how to diagnose common problems. For an overview of all capping methods, see our guide to the bottle capping machine working principle.
What Is a ROPP Cap?
A ROPP cap is a thin aluminium shell with:
- A smooth, unthreaded skirt — threads are formed during capping
- A liner or wad inside the top, which seals against the bottle mouth when compressed
- A perforated pilfer band at the bottom, connected to the cap by small bridges
When the cap is opened for the first time, the bridges break and the pilfer band stays on the neck, providing visible tamper evidence.
The Bottle Neck Finish
ROPP caps are used on bottles with a specific neck finish:
- External threads on the neck, which the cap is rolled onto
- A locking ring (bead) below the threads, under which the pilfer band is tucked
- A smooth sealing surface at the bottle mouth for the liner to seal against
Bottle and cap dimensions must be compatible, so ROPP caps and bottles are specified together.
The Core Working Principle
A ROPP capping head performs three actions on each bottle:
- Top load (axial pressure) — a pressure block presses the cap down firmly onto the bottle, compressing the liner against the bottle mouth to create the seal.
- Thread rolling — while the cap is held down, threading rollers press against the cap skirt and travel around it, following the bottle’s threads. This permanently forms matching threads in the soft aluminium.
- Pilfer-proof rolling — a pilfer-proof roller presses the pilfer band inward under the bottle’s locking ring, so that the band will break away when the cap is twisted open.
The result is a cap that is tightly sealed, cannot be removed without breaking the band and has threads perfectly matched to the bottle.
Inside the ROPP Capping Head
Pressure block
A spring-loaded or pneumatically controlled block that applies top load to the cap. Top load must be high enough to compress the liner and hold the cap steady during rolling, but not so high that it damages the bottle or cap.
Threading rollers
Usually two threading rollers mounted on spring-loaded arms. As the head rotates, centrifugal force or cams bring the rollers inward. They press the aluminium into the bottle threads, starting at the top of the thread and following its path down.
Pilfer-proof rollers
Usually one or two rollers positioned lower on the head. They roll the bottom of the cap inward under the locking ring.
Head rotation
The capping head spins around the stationary bottle (or, on some designs, the bottle is rotated). Roller pressure, spin speed and dwell time together decide how well threads and pilfer bands are formed.
Step-by-Step ROPP Capping Process
Step 1: Bottle infeed
Filled bottles arrive from the filler — for example, our volumetric bottle liquid filler — on a conveyor. On automatic machines, a star wheel or infeed worm spaces and positions them.
Step 2: Cap feeding
ROPP caps are loaded into a hopper and fed by a vibratory bowl or elevator, which orients them open side down and delivers them along a chute.
Step 3: Cap placement
As each bottle passes, it picks a cap off the end of the chute, or a pick-and-place head places the cap on the bottle neck.
Step 4: Head descent and top load
The capping head descends and the pressure block presses the cap firmly down, compressing the liner.
Step 5: Thread and pilfer rolling
The head rotates. Threading rollers move in and roll the threads; pilfer-proof rollers tuck the band under the locking ring.
Step 6: Head lift and discharge
Rollers retract, the head lifts and the capped bottle moves on to the next station.
Types of ROPP Capping Machines
Semi-automatic ROPP capping machines
The operator places a capped bottle under the head and starts the cycle. Ideal for small batches and start-ups. See the Semi-Automatic Bottle ROPP Capping Machine and our semi-automatic ROPP capping machine.
Automatic single head machines
Bottles and caps are fed automatically, and a single head caps one bottle at a time. Suitable for small to medium output. See the Automatic Single Head Bottle ROPP Capping Machine.
Automatic multi-head rotary machines
Several heads on a rotating turret cap bottles continuously, delivering higher output with consistent quality:
- Automatic Four Head Bottle ROPP Capping Machine — medium output
- Six head machines — higher output
- Automatic Eight Head Bottle ROPP Capping Machine — high-speed lines
Machines that handle both screw and ROPP caps with appropriate heads are also available — see our bottle screw and ROPP capping machine.
ROPP vs Screw Capping
| Feature | ROPP Capping | Screw Capping |
|---|---|---|
| Cap material | Aluminium | Plastic or metal |
| Cap threads | Formed during capping | Pre-formed |
| Securing action | Rolling threads and pilfer band | Rotating to set torque |
| Tamper evidence | Built-in pilfer band | Requires separate band or seal |
| Key control | Top load and roller settings | Torque setting |
| Typical products | Pharma syrups, liquors, oils | Syrups, tablets, shampoos, food |
For more on screw capping, read the bottle screw capping machine working principle.
Applications of ROPP Capping
- Pharmaceutical syrups and oral liquids — widely used in pharmacies and hospitals
- Liquors and spirits — tamper evidence and premium appearance
- Edible oils and sauces
- Mineral water and beverages in some markets
- Chemicals and agrochemicals where tamper evidence is needed
ROPP Capping in a Syrup Line
A typical pharmaceutical syrup line includes:
- Bottle unscrambling — using a bottle unscrambler
- Bottle cleaning
- Filling
- ROPP capping
- Measuring cup placement — on an automatic measuring cup placement machine
- Induction sealing (where foil liners are used) — on an induction sealing machine
- Labelling — on labeling machines for round bottles
For the full line process, see the automatic liquid syrup filling machine working principle.
Key Settings and Their Effects
| Setting | Too Low | Too High |
|---|---|---|
| Top load | Poor liner compression, leaks | Damaged caps or bottles, deformed liners |
| Threading roller pressure | Shallow threads, loose caps | Cut or torn aluminium, high removal torque |
| Threading roller start position | Threads not fully formed | Rollers hit shoulder, cap damage |
| Pilfer roller pressure | Band not tucked, weak tamper evidence | Band breaks prematurely, cap damage |
| Pilfer roller height | Band not under locking ring | Rolling on glass, damage |
| Head speed | Incomplete rolling | Uneven or damaged threads |
Quality Checks for ROPP Caps
- Visual inspection: threads clearly formed, cap straight, no cuts or creases, pilfer band neatly tucked
- Removal torque: the cap should open with acceptable force and the band should break as intended
- Leak testing: bottles inverted or vacuum-tested to confirm the liner seals
- Pilfer band check: band separates cleanly on opening and stays on the neck
- Cap height and squareness: consistent across all heads on multi-head machines
Troubleshooting Common ROPP Problems
| Problem | Likely Cause | Corrective Action |
|---|---|---|
| Leaking bottles | Low top load, damaged liner, poor bottle finish | Increase top load, check liners and bottles |
| Loose caps | Shallow threads from low roller pressure | Increase threading roller pressure |
| Cut or torn caps | Excessive roller pressure, worn rollers | Reduce pressure, replace rollers |
| Pilfer band not tucked | Pilfer roller too high or low pressure | Adjust height and pressure |
| Band breaks during capping | Excessive pilfer roller pressure | Reduce pressure |
| Tilted caps | Poor pick-off or bottle neck variation | Adjust pick-off, check bottles |
| Variation between heads | One head out of adjustment | Adjust and verify each head |
Glass vs PET Bottles
ROPP caps are applied to both glass and PET bottles, but the two behave differently:
- Glass bottles are rigid and can withstand higher top load, but neck finish variation and chipping must be watched carefully.
- PET bottles are lighter and more flexible. Excessive top load can deform the neck or shoulder, so top load is usually lower and bottle support more important.
Settings that work for one bottle type should never be assumed to work for another — each combination of bottle and cap should be set up and verified separately.
Changeover Between Cap and Bottle Sizes
When switching formats, operators typically:
- Clear the machine of caps and bottles from the previous batch
- Change star wheels, guides and cap chute parts
- Fit or adjust the capping head for the new cap diameter
- Set head height, top load and roller positions for the new neck finish
- Run trial bottles and check threads, pilfer band and removal torque
- Record settings and obtain approval before production
Labelled change parts and recorded settings for each format keep changeovers quick and consistent.
Maintenance Tips
- Inspect threading and pilfer rollers for wear and replace them before they cut caps
- Check springs and roller arms for consistent pressure
- Verify top load regularly
- Clean aluminium dust and debris from heads and turret
- Keep change parts for each bottle and cap size organised and labelled
- On multi-head machines, check every head during in-process checks
Choosing a ROPP Capping Machine
- Output — semi-automatic, single head or multi-head rotary
- Cap and bottle sizes — change parts for all formats
- Bottle material — glass or PET, which affects top load
- Line integration — matching filler speed
- Flexibility — whether screw caps will also be needed
- GMP requirements — for pharmaceutical products
- Service and spare parts — especially rollers and springs
Explore our capping machines, the capping machine for glass and PET bottles range and all capping machines on Harsiddh Engineering. For tips on getting the most from capping equipment, read optimizing production efficiency with advanced capping machines.
Frequently Asked Questions
What does ROPP stand for? Roll-on pilfer-proof — an aluminium cap whose threads are rolled on during capping and which has a tamper-evident band.
How does a ROPP capping machine work? A pressure block holds the cap down while threading rollers form threads in the aluminium and pilfer-proof rollers tuck the band under the bottle’s locking ring.
Why are ROPP caps used for syrups? They provide a reliable seal and clear tamper evidence, which are important for pharmaceutical products.
What is the difference between ROPP and screw caps? Screw caps have pre-formed threads and are tightened to a torque; ROPP caps are unthreaded and formed onto the bottle by rollers.
What causes leaking ROPP caps? Usually low top load, damaged liners or poor bottle neck finish.
Need a ROPP capping machine for your line? Contact our team or send an inquiry to discuss your bottles and caps.