
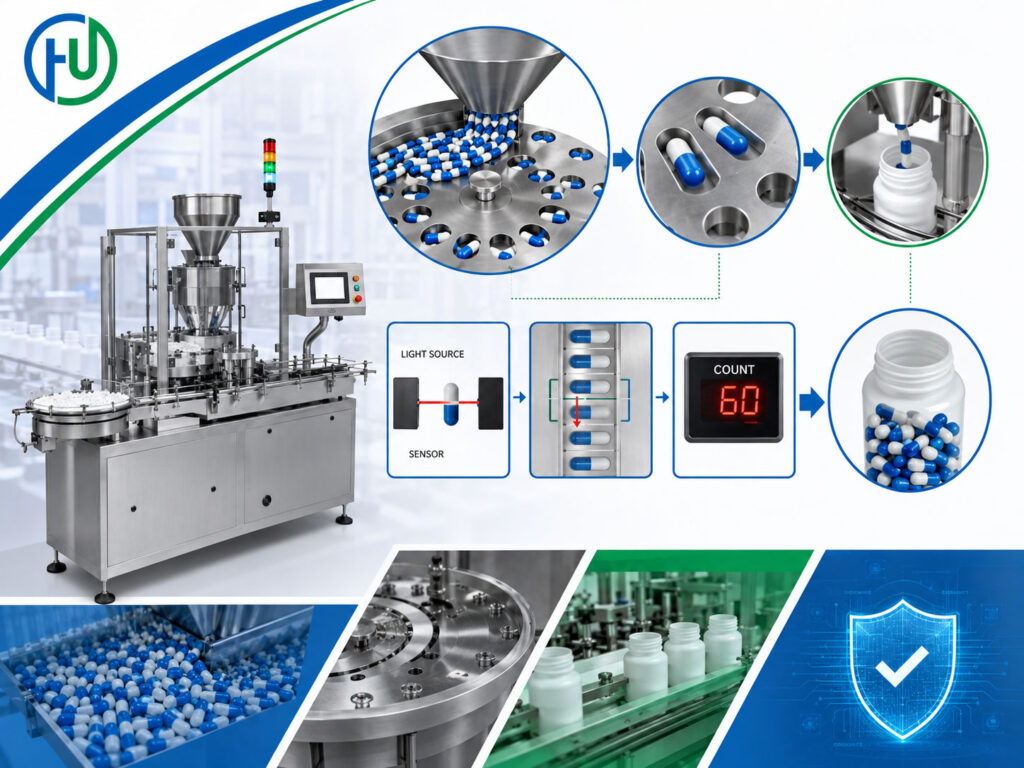
When a patient opens a bottle labelled “60 capsules”, they expect 60 capsules, not 59, not 61, and certainly not 58 whole capsules and a few broken halves. For pharmaceutical and nutraceutical manufacturers, the count on the label is a legal and quality commitment, and it has to be met on every bottle, shift after shift.
The capsule counting machine is what makes that possible. Modern machines count capsules electronically, at high speed and with very low error rates, by turning a heap of loose capsules into a steady stream of individual capsules that can each be detected by a sensor.
This article looks closely at how the counting itself works: how capsules are separated, how sensors see them, how the controller avoids miscounts and how count accuracy is verified. For an overview of the full bottling process, including encapsulation, see our capsule filling machine working principle.
Why Counting Capsules Is a Challenge
Capsules seem easy to count, but several properties make accurate high-speed counting difficult:
| Capsule Property | Counting Challenge |
|---|---|
| Smooth, glossy shells | Capsules slide and roll, sometimes overlapping |
| Elongated shape | Must travel lengthwise to pass sensors one at a time |
| Low weight | Light capsules bounce and can be affected by air flow |
| Sensitivity to humidity | Soft, sticky shells in humid conditions; brittle shells in dry conditions |
| Static charge | Capsules can cling to trays and each other |
| Range of sizes | From large sizes to very small sizes on the same machine |
| Possible defects | Dented, split or empty capsules and loose powder |
The counting machine’s design addresses each of these points.
The Core Principle: Separate, Then Detect
Every electronic capsule counter works on two simple ideas:
- Separate the capsules so that they move in single file with gaps between them.
- Detect each capsule as it passes a sensor and add one to the count.
If separation is good, detection is easy and accurate. Most counting errors come from poor separation: two capsules passing the sensor together or so close that they look like one.
Stage 1: Controlled Feeding from the Hopper
Bulk capsules are loaded into a hopper above the machine. The hopper outlet has an adjustable gate that controls how many capsules flow onto the first vibratory tray.
- Too many capsules create a thick layer on the trays, causing overlapping and stacking.
- Too few capsules leave the channels underfed, slowing output.
Some machines use a level sensor on the trays to adjust the hopper feed automatically and keep a steady flow.
Stage 2: Vibratory Separation
The capsules move across a series of stepped vibratory trays, usually two or three. Each tray has its own electromagnetic vibrator and its own amplitude setting.
The principle is progressive acceleration:
- The first tray moves capsules forward slowly and spreads them into a thinner layer.
- The second tray vibrates more strongly, moving capsules faster, so gaps open up between them.
- The final tray moves capsules faster still, delivering a single, well-spaced layer to the channels.
Because each tray runs faster than the one before, capsules are pulled apart rather than pushed together, a bit like cars spreading out as they accelerate onto a motorway.
Stage 3: Channelling into Single File
The final tray feeds a channel plate: a series of grooves, each just wide enough for one capsule lying lengthwise. The channels:
- Turn capsules so they travel end to end
- Prevent two capsules travelling side by side
- Keep each lane separate so capsules fall one at a time
Channel width and depth are matched to the capsule size. Changing capsule size usually means fitting a different channel plate. A plate that is too wide allows side-by-side capsules; one that is too narrow causes jams.
Stage 4: Optical Detection
At the end of each channel, capsules fall freely through a sensor window. This is where counting happens.
How the sensor works
Most capsule counters use infrared or photoelectric sensors arranged across the falling path:
- A row of light emitters sends beams across the fall path.
- Receivers on the opposite side detect the light.
- When a capsule falls through, it blocks some of the beams for a brief moment.
- The sensor electronics register this interruption as an object passing.
Using an array of beams rather than a single beam makes detection reliable regardless of where in the window the capsule falls.
Signal processing
The controller does more than just count interruptions. It analyses each signal to decide whether it represents one capsule:
- Duration of interruption – a capsule of a known size blocks the beams for a predictable time as it falls.
- Size of interruption – how many beams are blocked indicates the object’s size.
- Gap between objects – two signals very close together can be checked to ensure two capsules have been counted.
By comparing each signal with what a good capsule looks like, the system can identify:
- Single capsules – counted normally
- Fragments or loose powder clumps – signals too small, flagged as possible defects
- Doubles – signals too long or too large, which may indicate two capsules together
What the machine does with a suspect signal, whether it counts, alarms or rejects the bottle, depends on the sensor system and its configuration.
Dust compensation
Capsule dust can gradually coat sensor windows and reduce light levels. Many sensor systems monitor their own light levels and compensate automatically, or raise an alarm when cleaning is needed. Regular cleaning remains essential.
Stage 5: Totalising and Gating
Counts from all channels are added together for the current bottle. When the total reaches the set count:
- A gate closes or switches over, so further capsules from all channels are directed to a second chamber for the next bottle.
- The counted capsules wait in a pre-count chamber until the bottle is ready.
- When the bottle is positioned under the funnel, the chamber opens and the capsules drop in.
The gate must act very quickly so that a capsule already falling is directed to the correct chamber. Fast-acting gates and good timing are key to accuracy at high speeds.
Stage 6: Filling the Bottle
The counted capsules fall through a funnel into the bottle. The funnel guides them into the bottle neck without bouncing out. Bottles are positioned by a stopper system or star wheel on the conveyor and then released once filled.
Empty bottles reach the counter via a bottle unscrambler, such as our Automatic Bottle Unscramblers or the bottle unscrambler on Harsiddh Engineering, and are often air-cleaned first, using an Automatic Bottle Air Jet and Vacuum Cleaning Machine or the automatic bottle air-jet and vacuum cleaning machine.
Capsule Counting Machines from Harsiddh
- Automatic Capsule Counting and Filling Machine
- Automatic Tablet Counting and Filling Machine, for both tablets and capsules
- Tablet and capsule counting and filling machine
Browse the tablet and capsule counting and filling machines category and the tablet and capsule counting and filling line. For tablet-specific considerations, read our tablet filling machine working principle.
Environmental Factors: Humidity and Static
Humidity
Hard gelatin capsules contain moisture as part of their structure. In high humidity they absorb more, becoming soft and sticky, which can cause them to cling to trays and channels and slow or block feeding. In very low humidity they lose moisture and become brittle, which can lead to cracking when they drop. HPMC (vegetarian) capsules behave differently and are generally less sensitive to low humidity. Room conditions for counting should follow the capsule supplier’s recommendations and your product requirements.
Static electricity
In dry conditions, capsules rubbing against trays and each other can build up a static charge. Charged capsules cling to surfaces, stick together or jump unpredictably, all of which disturb counting. Static is reduced by:
- Maintaining suitable room humidity
- Proper grounding of the machine
- Using anti-static measures such as ionisers where needed
- Choosing suitable contact materials
Verifying Count Accuracy
Even with excellent sensors, count accuracy must be checked:
- Start-up verification – run a set of bottles and count the contents manually.
- Challenge test – run a known number of capsules through the machine and confirm the machine count matches.
- In-process checks – sample bottles at set intervals and count by hand or by weight.
- Checkweighing – an in-line checkweigher rejects bottles whose weight indicates a missing or extra capsule. This works best when capsule weight variation is small compared with the weight of a single capsule.
- Visual inspection – check filled bottles for broken capsules, for example on a bottle visual inspection table.
Frequencies and acceptance criteria should be defined in your quality procedures.
After Counting: Closing the Bottle
Counted bottles move on to capping and sealing:
- Capping – on an Automatic Six Head Bottle Screw Capping Machine, a bottle screw and ROPP capping machine or, for small batches, a semi-automatic screw capping machine
- Induction sealing – a foil liner sealed to the bottle lip on an Automatic Induction Cap Sealing Machine or an induction sealing machine. The seal acts as a moisture barrier, which matters for humidity-sensitive capsules, and gives clear tamper evidence when the bottle is first opened.
- Labelling – on a bottle sticker labeling machine
Key Settings and Their Effect on Counting
| Setting | What It Controls | Effect If Wrong |
|---|---|---|
| Hopper gate | Supply to trays | Overlapping or starved channels |
| Tray vibration amplitudes | Separation and speed | Doubles, or capsules bouncing out |
| Channel plate size | Single-file travel | Side-by-side capsules or jams |
| Sensor sensitivity and size limits | What counts as one capsule | Missed counts, fragments counted |
| Count setpoint | Capsules per bottle | Wrong pack count |
| Gate timing | Switching between bottles | Capsules in the wrong bottle |
| Conveyor and stopper timing | Bottle position under funnel | Spillage |
Troubleshooting Capsule Counting Errors
| Symptom | Likely Cause | Corrective Action |
|---|---|---|
| Occasional under-count | Two capsules passing together | Reduce feed, adjust vibration for better spacing |
| Occasional over-count | Fragments or powder clumps detected as capsules | Adjust size limits, inspect capsule quality, clean sensors |
| Counts drifting over shift | Dust building up on sensors | Clean sensors more often, check extraction |
| Capsules sticking on trays | High humidity, static | Adjust room humidity, check grounding |
| Capsules jamming in channels | Wrong plate, dented capsules | Fit correct plate, check incoming capsules |
| Cracked capsules in bottles | Low humidity, long drop | Adjust humidity, shorten drop |
| Capsules in wrong bottle | Gate timing | Adjust gate and chamber timing |
Maintenance Tips
- Clean sensor windows at regular intervals during production.
- Check and empty dust extraction filters.
- Inspect vibrators, springs and tray mountings.
- Verify gates and chambers open and close cleanly.
- Keep channel plates for each capsule size clean, labelled and stored safely.
- Carry out challenge tests with a known count at defined intervals.
Frequently Asked Questions
What is the working principle of a capsule counting machine? Vibratory trays separate bulk capsules into single file through channels. Each capsule falls through an optical sensor that detects and counts it. When the set count is reached, a gate diverts capsules to the next chamber and the counted capsules drop into the bottle.
How does the machine avoid counting two capsules as one? By separating capsules well with progressive vibration and channels, and by analysing the size and duration of each sensor signal.
Can capsule counters detect broken capsules? Many sensor systems can identify signals that are too small for a whole capsule and flag them, depending on the system.
Why does humidity affect capsule counting? Humid conditions make capsules soft and sticky; dry conditions make them brittle and prone to static. Both affect feeding and counting.
Can the same machine count tablets? Yes. Electronic counters handle tablets and capsules with the appropriate channel plates and settings.
Looking for an accurate capsule counting machine? Contact our team or send an inquiry with your capsule sizes, pack counts and bottle details.