
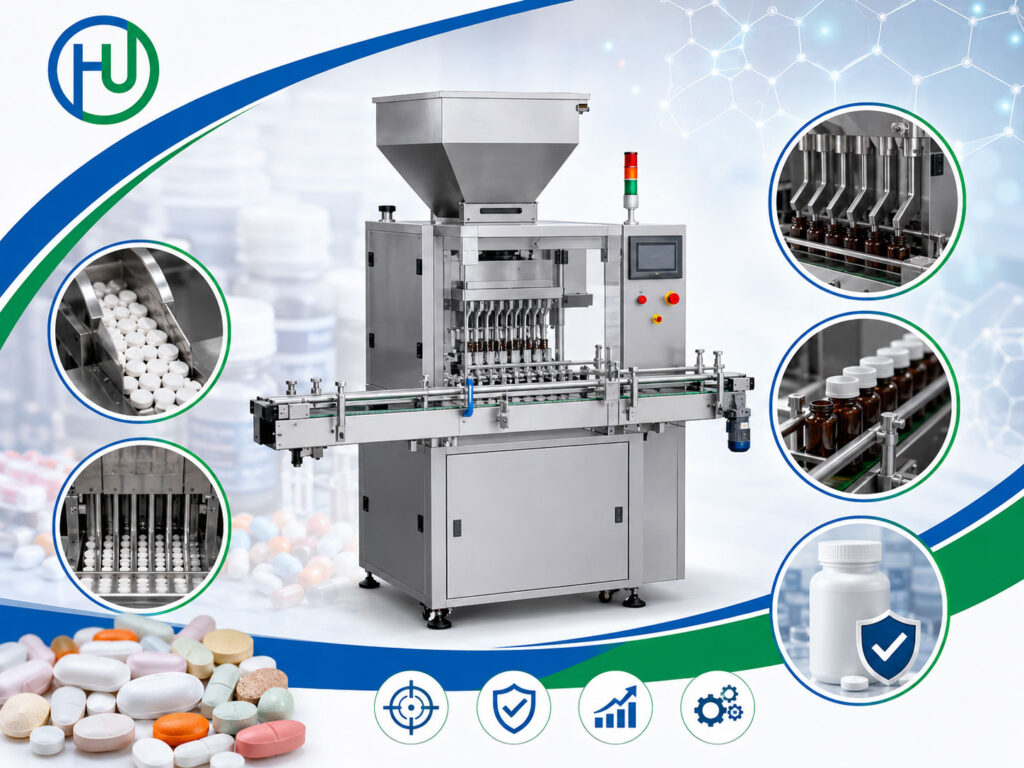
Tablets are the most widely used solid dosage form. Painkillers, vitamins, antibiotics, antacids, heart medicines and nutritional supplements are all supplied as tablets, and a large share of them are packed in bottles and jars rather than blister packs. Packs might hold a handful of tablets or several hundred, and every bottle must contain exactly the number stated on the label.
A tablet filling machine, also called a tablet counting and filling machine, does this job automatically. It takes bulk tablets, counts them precisely and drops the counted tablets into each bottle, ready for capping and sealing.
In this article, we explain the working principle of tablet filling machines, the different counting methods, how tablet shape and coating affect the process, how to control dust and breakage, how the machine fits into a complete bottling line, and how to troubleshoot common problems.
If you pack capsules as well, see our companion articles on the capsule filling machine working principle and the capsule counting machine working principle.
What a Tablet Filling Machine Has to Achieve
A good tablet filler must deliver:
- Exact count – every bottle contains the declared number of tablets
- Gentle handling – no chipping, breaking or capping of tablets
- Clean operation – minimal dust, which can affect sensors and cleanliness
- Flexibility – quick changeovers between tablet sizes, counts and bottles
- Steady output – matched to the capper, sealer and labeller downstream
Counting Methods Used in Tablet Filling
Electronic (sensor) counting
The most widely used method in modern lines. Tablets are separated by vibration into single-file channels and counted by optical sensors as they fall. Electronic counters handle a wide range of tablet sizes and shapes with simple change parts and can count to any number set on the control panel.
Slat counting
A moving belt of slats with pockets, one tablet per pocket, carries tablets past a discharge point. The count is set by the number of pockets per bottle. Slat counters handle tablets gently but need change slats for each tablet size.
Disc (plate) counting
A rotating plate with holes, each sized for one tablet, picks up tablets from a hopper. The plate carries a set number of tablets to a discharge chute. These are simple machines suited to small batches and limited sizes.
Weight counting
Bottles are filled and weighed; the count is inferred from the average tablet weight. This is used mainly for larger counts and some non-pharmaceutical products, where weight variation is tightly controlled.
Electronic counting is the focus of the rest of this article, because it is the most common choice for pharmaceutical and nutraceutical bottling.
Main Components of an Electronic Tablet Filling Machine
- Bulk hopper – holds tablets and releases them at a controlled rate through an adjustable outlet.
- Vibratory trays – typically several stepped trays, each with its own vibrator, that spread tablets into a single layer and move them forward.
- Channel plates – grooved plates that guide tablets into separate lanes.
- Counting sensors – optical sensors at the end of each lane that detect each falling tablet.
- Pre-count chambers and gates – hold counted tablets until a bottle is ready, then release them.
- Discharge funnel – guides tablets into the bottle neck.
- Bottle conveyor and positioning system – stops each bottle under the funnel.
- Dust extraction – draws dust away from sensors and the counting area.
- Control panel (HMI) – sets count, vibration levels and speed; displays totals and alarms.
- Reject system – diverts bottles with a count error, if fitted.
Step-by-Step: How a Tablet Filling Machine Works
Step 1: Bottle supply
Empty bottles are fed onto the conveyor by a bottle unscrambler, for example our Automatic Bottle Unscramblers or the bottle unscrambler on Harsiddh Engineering. Bottles are often cleaned with air first, using an Automatic Bottle Air Jet and Vacuum Cleaning Machine or the automatic bottle air-jet and vacuum cleaning machine.
Step 2: Hopper feeding
Bulk tablets are loaded into the hopper. An adjustable gate controls how many tablets flow onto the first vibratory tray. Too many tablets cause piling and overlapping; too few slow the machine.
Step 3: Separation by vibration
The first tray vibrates and moves tablets forward while spreading them out. Each following tray usually vibrates slightly faster than the one before, so tablets accelerate and gaps open up between them. By the last tray, tablets are moving in a single layer.
Step 4: Channelling into lanes
The final tray feeds tablets into a channel plate with grooves matched to the tablet size and shape. Each groove forms a lane in which tablets travel one behind another.
Step 5: Counting
At the end of each lane, tablets fall one at a time through an optical sensor. Each tablet interrupts a light beam, and the control system adds one to the count for that bottle. Counts from all lanes are added together.
Depending on the sensor system, the machine may also detect fragments or tablets that are too small and raise an alarm or reject the bottle.
Step 6: Pre-count and gating
Counted tablets collect in a pre-count chamber above the bottle. When the target count is reached, a gate stops further tablets entering that chamber and diverts them to the next one. This means the machine can count the next bottle’s tablets while the current bottle is being filled, keeping output steady.
Step 7: Dropping into the bottle
Once a bottle is in position under the funnel, the chamber opens and the counted tablets drop into the bottle. Funnel design keeps the drop gentle and guides tablets cleanly through the bottle neck.
Step 8: Discharge and next bottle
The filled bottle moves on along the conveyor and the next bottle is positioned. The cycle repeats continuously.
How Tablet Characteristics Affect Filling
Not all tablets behave alike. The machine is set up for each product.
| Tablet Characteristic | Effect on Filling | What to Adjust |
|---|---|---|
| Round, flat tablets | Usually feed easily | Standard channels |
| Oval or capsule-shaped (caplets) | Must travel lengthwise | Narrow channels matched to width |
| Large tablets | Slower flow, bigger drop forces | Wider channels, gentler drop |
| Small tablets | Can travel side by side or bounce | Narrow channels, careful vibration |
| Film-coated tablets | Smooth, flow well, coating can chip | Gentle handling, reduced drop height |
| Sugar-coated tablets | Heavier, can chip | Lower vibration, soft contact surfaces |
| Uncoated or friable tablets | Produce dust, can break | Dust extraction, gentle vibration |
| Effervescent or hygroscopic tablets | Sensitive to moisture | Low humidity, prompt capping |
| Chewable tablets | Softer, may stick | Clean trays often, control humidity |
Dust and Breakage Control
Dust and broken tablets cause two problems: count errors, because fragments can be counted as tablets or dust can blind sensors, and quality complaints, because customers find broken tablets or powder in the bottle.
Good practice includes:
- Setting vibration no higher than needed
- Keeping drop heights short and funnels smooth
- Fitting effective dust extraction at the trays and sensors
- Cleaning sensors and channels at regular intervals during the shift
- Using tablets that meet hardness and friability specifications before packing
Tablet Filling Machines from Harsiddh
- Automatic Tablet Filling Machine
- Automatic Tablet Counting and Filling Machine
- Automatic Capsule Counting and Filling Machine
- Tablet and capsule counting and filling machine on Harsiddh Engineering
Browse the tablet and capsule counting and filling machines category and the complete tablet and capsule counting and filling line.
The Complete Tablet Bottling Line
- Bottle unscrambler – orients and feeds empty bottles
- Air jet cleaning – removes dust and particles
- Tablet counting and filling – electronic counting into bottles
- Desiccant or cotton insertion (where required) – protects against moisture and movement
- Capping – screw caps on a bottle screw and ROPP capping machine or a linear capping machine
- Induction sealing – foil liner sealed to the bottle lip, using an Automatic Continuous Induction Bottle Sealing Machine or an induction sealing machine
- Labelling – using labeling machines for round bottles
- Checkweighing – confirms count by weight and rejects out-of-limit bottles
- Cartoning and packing
Every machine should run at a speed matched to the counter, with short buffers so a brief stop at one station does not stop the whole line.
Key Settings and Their Effects
| Setting | What It Controls | Effect If Wrong |
|---|---|---|
| Hopper gate opening | Tablet supply to trays | Overloaded trays or slow output |
| Vibration level per tray | Spreading and acceleration | Overlapping tablets or tablet damage |
| Channel plate size | Single-file lanes | Jams or side-by-side tablets |
| Sensor sensitivity | Detecting each tablet | Missed counts or dust triggering counts |
| Count per bottle | Pack quantity | Wrong count |
| Gate timing | Separation between bottles | Tablets in the wrong bottle |
| Conveyor speed and stopper | Bottle position | Spillage, missed bottles |
Checking Count Accuracy
- At start-up, run several bottles and hand count the contents
- At set intervals during production, check sample bottles by counting or by weight against a known average tablet weight
- Use an in-line checkweigher to catch bottles with missing or extra tablets
- Visually inspect filled bottles for broken tablets or foreign items, for example on a bottle visual inspection table
- Record results in the batch documentation
The sampling frequency and acceptance limits should be defined in your quality procedures.
Changeover Between Products
- Line clearance: remove all tablets, bottles, labels and printed materials from the previous batch
- Clean the hopper, trays, channels, sensors, chambers and funnels
- Fit the channel plate for the new tablet size
- Adjust bottle guides and the stopper system for the new bottle
- Set the new count, vibration and speed
- Run test bottles and verify counts before releasing production
Recorded settings for each product and clearly labelled change parts make changeovers faster and more consistent.
Troubleshooting Common Problems
| Problem | Likely Cause | Corrective Action |
|---|---|---|
| Over-count or under-count | Overlapping tablets, dirty sensors, fragments | Adjust vibration and feed, clean sensors, check tablet quality |
| Tablets jamming in channels | Wrong channel size, irregular tablets | Fit correct plate, inspect tablets |
| Chipped or broken tablets | High vibration, long drop | Reduce vibration, shorten drop, soften contact points |
| Tablets bouncing out of bottle | Funnel misaligned, drop too fast | Align funnel, adjust drop |
| Excess dust | Friable tablets, weak extraction | Improve extraction, check friability |
| Tablets sticking on trays | Humidity, soft tablets | Control room humidity, clean trays |
| Machine slow | Trays underfed, conservative settings | Open hopper gate, optimise vibration |
Maintenance Tips
- Clean optical sensors regularly during production, not only at the end of the batch.
- Inspect vibrators and tray mountings for wear and loosening.
- Check dust extraction filters.
- Verify count accuracy with a known number of tablets at start-up.
- Keep channel plates and change parts clean, labelled and stored together.
- Clean thoroughly between products to prevent cross-contamination and mix-ups.
How to Choose a Tablet Filling Machine
- Tablet types and sizes – round, oval, coated, uncoated
- Count range per bottle
- Output and number of channels
- Bottle sizes and changeover frequency
- Dust control and cleanability
- Line integration – desiccant insertion, capping, sealing, labelling
- GMP and documentation
Frequently Asked Questions
What is the working principle of a tablet filling machine? Bulk tablets are spread out by vibratory trays, guided into single-file channels and counted by optical sensors as they fall. When the set count is reached, the counted tablets are dropped into a bottle.
Which counting method is most common? Electronic sensor counting, because it handles a wide range of tablet sizes and counts with simple change parts.
Why do tablet counts go wrong? Usually because tablets overlap in the channels, sensors are dusty, or broken fragments are counted.
Can a tablet filling machine also count capsules? Yes. Most electronic counters handle both tablets and capsules with suitable channel plates and settings.
Why are induction seals used on tablet bottles? They add a moisture barrier and tamper evidence under the cap.
Planning a tablet bottling line? Contact our team or send an inquiry with your tablet sizes, pack counts and bottle details.