
Hard capsules are one of the most popular oral dosage forms in the world. They are easy to swallow, mask unpleasant tastes, protect sensitive ingredients and can be made in many colours and sizes for branding. Millions are produced and packed every day for prescription medicines, over-the-counter products and nutraceuticals.
The term “capsule filling machine” is used in two different ways in the pharmaceutical industry:
- Encapsulation machines – which fill powder, pellets or granules into empty capsule shells and close them.
- Capsule bottle filling machines – which count finished capsules and fill them into bottles or jars for sale.
Both are essential, but they happen at different stages of production. In this article, we explain the working principle of each, then look in detail at how a complete capsule bottle filling line works, including counting, capping, sealing and labelling.
Part 1: Encapsulation – Filling Capsule Shells
The hard capsule
A hard capsule has two parts: a longer body and a shorter cap. Empty capsules are supplied pre-joined (lightly locked together) so they can be handled. The encapsulation machine separates them, fills the body and rejoins the two halves.
The encapsulation working principle
Whether manual, semi-automatic or fully automatic, encapsulation follows the same sequence:
- Rectification (orientation) – empty capsules are fed from a hopper and turned so that all bodies point the same way.
- Separation – each capsule is placed in a two-part bushing (segment). Vacuum pulls the body down into the lower part while the cap is held in the upper part.
- Filling (dosing) – the open body receives the fill material.
- Rejecting – capsules that did not separate are removed.
- Closing – the cap and body are aligned and pushed together until they lock.
- Ejection – the closed, filled capsules are pushed out of the machine.
- Polishing and inspection – capsules are cleaned of surface powder and checked.
How powder is dosed into capsules
The two most common dosing principles are:
- Tamping (dosing disc) – a disc with holes passes under a powder bed. Tamping pins press powder into each hole several times to form a compact plug, which is then pushed into the capsule body.
- Dosator – a hollow tube dips into a powder bed. Powder enters the tube and is compressed by an inner piston to form a plug, which is then ejected into the capsule body.
Pellets and granules are often dosed by volumetric chambers or slides rather than compressed plugs.
Types of encapsulation machines
| Type | How It Works | Typical Use |
|---|---|---|
| Manual | Operator loads, levels and closes capsules in plates | Very small batches, R&D |
| Semi-automatic | Machine orients and separates; operator assists filling and closing | Small to medium batches |
| Fully automatic | All steps performed on an indexing turret | Commercial production |
Fill weight in encapsulation depends on capsule size, powder density, compression and machine settings, and is checked at regular intervals during production.
Part 2: Filling Finished Capsules into Bottles
Once capsules have been made, polished and inspected, they need to be packed. Blister packs are common for some markets, but bottles and jars are widely used for nutraceuticals, larger pack counts and many prescription medicines. This is where a capsule counting and filling machine comes in.
The working principle in brief
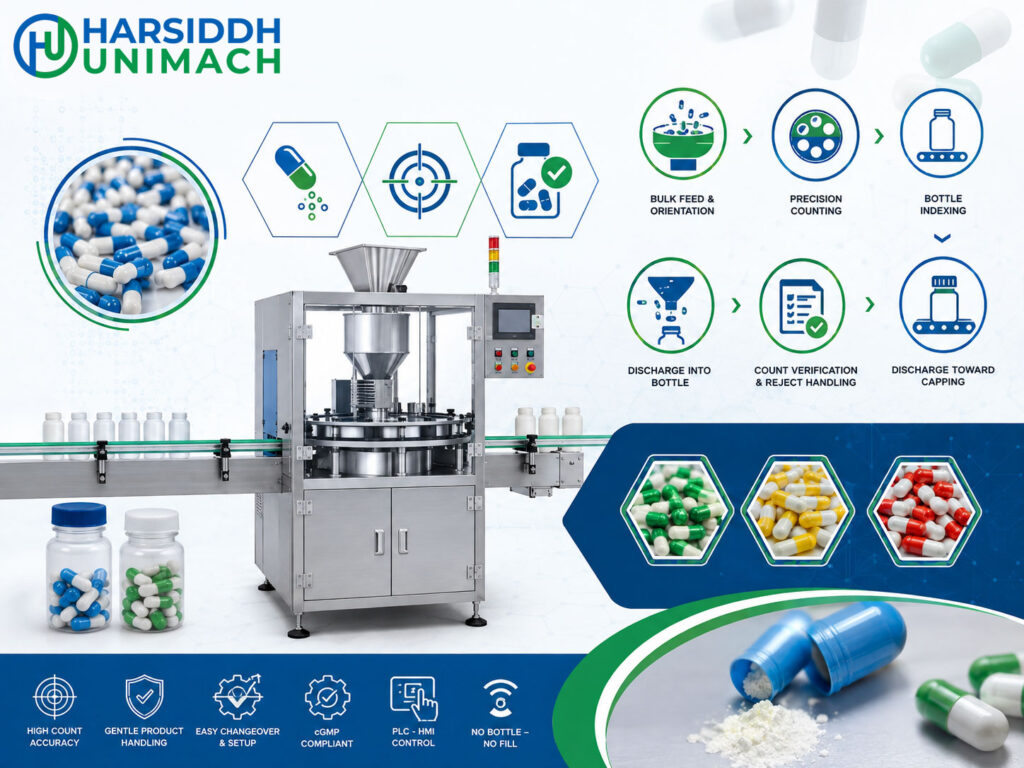
A capsule bottle filling machine counts a precise number of capsules and drops them into each bottle. Counting is usually done with electronic sensors: capsules are vibrated into separate channels and fall one at a time past optical sensors that count each one. When the target count is reached, a gate closes and the counted capsules drop into the bottle below.
For a full explanation of the counting technology, read our capsule counting machine working principle.
Main components of a capsule counting and filling machine
- Capsule hopper – stores bulk capsules and feeds them at a controlled rate.
- Vibratory feeder trays – usually several stepped trays that spread capsules out and move them forward in a single layer.
- Channels or tracks – guide capsules into separate lanes so they fall one at a time.
- Counting sensors – optical (infrared or photoelectric) sensors in each lane detect and count every capsule that passes.
- Gates and funnels – hold the counted capsules and release them into the bottle.
- Bottle conveyor and stopper system – positions bottles under the funnels.
- Dust extraction – removes capsule dust and fragments that could interfere with sensors.
- Control panel – sets the count, speed and vibration levels, and shows production totals.
Step-by-step bottle filling process
Step 1: Bottle feeding
Empty bottles are fed onto the conveyor by a bottle unscrambler, such as our Automatic Bottle Unscramblers, which orients them upright (see also the bottle unscrambler on Harsiddh Engineering). Bottles may pass through an air cleaner, such as the automatic bottle air-jet and vacuum cleaning machine, to remove dust and particles.
Step 2: Capsule feeding
Bulk capsules are loaded into the hopper. A controlled outlet feeds them onto the first vibratory tray. The vibration spreads the capsules out and moves them forward. Each following tray vibrates at its own setting, gradually separating capsules into a single layer.
Step 3: Channelling
At the end of the trays, capsules enter a series of grooved channels. Each channel guides capsules into single file so that they fall one at a time.
Step 4: Counting
As each capsule falls from the end of its channel, it passes through an optical sensor. The sensor detects the interruption of its light beam and adds one to the count. The control system totals the counts from all channels for the bottle being filled.
Modern sensors can also detect capsules that are broken or the wrong size, depending on the system, and can flag or reject those bottles.
Step 5: Gating and filling
When the target count is reached, the gate for that bottle closes, temporarily holding back further capsules. The counted capsules fall through a funnel into the bottle. Then the next bottle moves into position and the gate opens again.
Some machines use a pre-count hopper: capsules for the next bottle are counted into a holding chamber while the current bottle is being filled, so there is no waiting time between bottles.
Step 6: Bottle discharge
Filled bottles move on along the conveyor to the next station.
Capsule counting and filling machines
- Automatic Capsule Counting and Filling Machine
- Automatic Tablet Counting and Filling Machine, which handles tablets and capsules
- Tablet and capsule counting and filling machine on Harsiddh Engineering
Browse the tablet and capsule counting and filling machines category and the tablet and capsule counting and filling line. If you also pack tablets, read our tablet filling machine working principle or see the Automatic Tablet Filling Machine.
The Complete Capsule Bottle Filling Line
A typical automatic line includes:
- Bottle unscrambler – orients and feeds bottles
- Air cleaning – removes dust from bottles
- Capsule counting and filling – electronic counting into bottles
- Desiccant or cotton insertion (where required) – protects capsules from moisture and movement
- Capping – screw caps, for example on an Automatic Four Head Bottle Screw Capping Machine, the bottle screw and ROPP capping machine or the semi-automatic screw capping machine for small batches
- Induction sealing – a foil liner sealed to the bottle lip for moisture protection and tamper evidence, using an Automatic Induction Cap Sealing Machine or an induction sealing machine
- Labelling – on a bottle sticker labeling machine or one of our labeling machines for round bottles
- Checkweighing and inspection – confirms the bottle contains the right number of capsules
- Cartoning and packing
Matching the speed of each machine to the counter keeps the line running smoothly without gaps or back-ups.
Why Moisture Protection Matters
Hard gelatin capsules are sensitive to humidity. Too much moisture makes them soft and sticky; too little makes them brittle. Many fill materials are also moisture-sensitive. That is why capsule bottling lines often include:
- Controlled room humidity and temperature
- Desiccant canisters or sachets in the bottle
- Induction-sealed foil liners under the cap
- Prompt capping after filling
The appropriate conditions depend on the capsule type (gelatin or HPMC) and the product, so always refer to product development data and your own quality procedures.
Key Settings for Capsule Counting and Filling
| Setting | What It Controls | Effect If Wrong |
|---|---|---|
| Hopper outlet | Rate of capsules entering the trays | Overloading or starving the trays |
| Tray vibration levels | Separation and forward speed | Capsules overlapping, double counts |
| Channel size | Single-file feeding | Jams or two capsules side by side |
| Sensor sensitivity | Detection of each capsule | Missed counts or false counts from dust |
| Count setting | Capsules per bottle | Wrong pack count |
| Gate timing | Clean separation between bottles | Capsules falling into the wrong bottle |
| Conveyor speed | Bottle positioning | Missed bottles, spillage |
Changeover Between Capsule Sizes and Products
Capsule bottling lines often run several products and pack sizes, so a quick, controlled changeover matters for output and for avoiding mix-ups. A typical changeover involves:
- Line clearance – removing every capsule, bottle, label and printed component from the previous batch
- Cleaning – emptying the hopper and cleaning trays, channels, sensors and funnels
- Changing channels or tray inserts to suit the new capsule size
- Adjusting conveyor guides and the bottle stopper system for the new bottle
- Setting the count and adjusting vibration levels for the new product
- Verifying counts by running test bottles and checking them manually before releasing the batch
Labelled change parts, recorded settings for each product and a written changeover checklist help operators complete this consistently and quickly.
Troubleshooting Common Problems
| Problem | Likely Cause | Corrective Action |
|---|---|---|
| Incorrect counts | Overlapping capsules, dust on sensors | Adjust vibration, clean sensors, check extraction |
| Capsules jamming in channels | Wrong channel size, deformed capsules | Fit correct channels, check capsule quality |
| Broken or dented capsules | Excessive drop height, harsh vibration | Reduce drop height, lower vibration |
| Capsules missing the bottle | Funnel misaligned, bottle not positioned | Align funnel, check stopper system |
| Slow output | Trays underfed, conservative settings | Increase feed rate, optimise vibration |
| Sticky capsules | High humidity | Improve room humidity control |
| Static build-up | Dry conditions, plastic contact parts | Use static control measures, check grounding |
Maintenance Tips
- Clean sensors and channels regularly; capsule dust is the most common cause of count errors.
- Check the dust extraction system and filters.
- Inspect vibratory trays for wear and correct mounting.
- Verify count accuracy at start-up and at regular intervals with a known number of capsules.
- Keep change parts for each capsule size and bottle labelled and stored together.
- Clean thoroughly between products to prevent mix-ups.
How to Choose a Capsule Filling Machine
For encapsulation
- Capsule sizes to be run
- Fill material – powder, pellets, granules or combinations
- Dosing principle – tamping or dosator
- Output – manual, semi-automatic or fully automatic
- Weight control and inspection features
For capsule bottle filling
- Capsule and tablet sizes to be counted
- Pack counts – from small packs to large bottles
- Number of channels and required output
- Bottle sizes and changeover needs
- Downstream integration – desiccant, capping, induction sealing, labelling
- Dust control and cleanability
- GMP documentation
Frequently Asked Questions
What is the working principle of a capsule filling machine? An encapsulation machine orients empty capsules, separates the cap from the body, fills the body with a measured dose and rejoins the two halves. A capsule bottle filling machine counts finished capsules with electronic sensors and drops the counted capsules into bottles.
What is the difference between capsule filling and capsule counting? Capsule filling (encapsulation) puts the medicine into the capsule shell. Capsule counting and filling puts a set number of finished capsules into a bottle.
How do electronic capsule counters count accurately? Vibratory trays separate capsules into single file, and optical sensors count each capsule as it falls past.
Why are desiccants and induction seals used in capsule bottles? Capsules and many fill materials are sensitive to moisture. Desiccants absorb moisture inside the bottle, and induction seals add a barrier and tamper evidence.
Can one machine count both tablets and capsules? Yes. Most electronic counting machines handle both, with change parts and settings for each product size.
Planning a capsule bottle filling line? Contact our team or send an inquiry with your capsule size, pack counts and bottle details.