
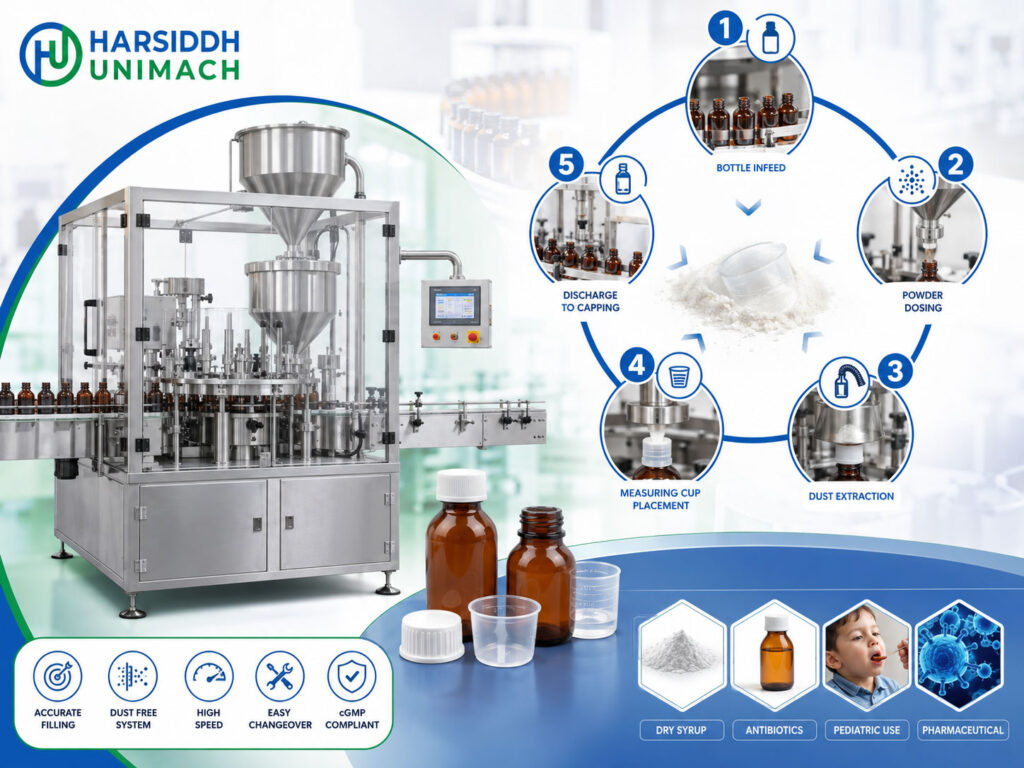
Many paediatric antibiotics and other oral medicines are not stable as liquids for long. The answer is dry syrup: a measured quantity of powder or granules in a bottle, which the pharmacist or patient reconstitutes by adding water up to a mark on the bottle. The result is an oral suspension that is easy to give to children and remains effective for the period stated on the label.
From a manufacturing point of view, dry syrup sits between two worlds. The container is a bottle, handled much like a liquid syrup bottle, but the product is a powder. That combination calls for a dedicated machine: the dry syrup filling machine, also known as a dry syrup powder filling machine.
In this article, we explain how a dry syrup filling machine works, step by step, how fill weight is controlled, why humidity and dust matter so much, and how the filler fits into a complete dry syrup line. For a wider look at powder dosing methods, see our guide to the powder filling machine working principle. If you are new to powder filling altogether, start with what is a powder filling machine and how does it work.
What Makes Dry Syrup Filling Different?
| Aspect | Liquid Syrup Filling | Dry Syrup Filling |
|---|---|---|
| Product | Liquid | Powder or granules |
| Dosing method | Piston, pump, gravity or flow meter | Auger or volumetric powder dosing |
| Main accuracy risk | Viscosity, foaming, temperature | Bulk density, flowability, humidity |
| Environment | Normal production room | Controlled humidity, dust extraction |
| Typical closure | ROPP or screw cap | ROPP or screw cap, often with induction seal |
| Reconstitution | Not required | Water added before use |
If you also fill liquid syrups, our article on the automatic liquid syrup filling machine working principle explains that process.
Main Components of a Dry Syrup Filling Machine
- Infeed conveyor – brings clean, empty bottles to the machine.
- Infeed worm or star wheel – spaces bottles and feeds them into the indexing system.
- Rotary indexing table or star wheel – moves each bottle precisely under the filling head and holds it stationary during filling.
- Powder hopper – stores the dry syrup powder above the dosing unit.
- Agitator – rotates inside the hopper to keep the powder moving and feed the auger evenly.
- Auger and auger tube – the dosing element; each revolution delivers a nearly fixed volume of powder.
- Servo or stepper drive – controls the number of auger revolutions precisely.
- Filling funnel or nozzle – guides powder into the bottle neck with minimal spillage.
- Level sensor and powder feeding system – keeps the hopper level within a band, sometimes with a screw feeder or vacuum transfer from a bulk container.
- Dust extraction points – remove airborne powder at the filling station.
- Outfeed conveyor – carries filled bottles onward to capping.
- Control panel – sets fill weight, speed and counts, with “no bottle, no fill” and safety interlocks.
Step-by-Step Working Principle
Step 1: Bottle preparation
Empty bottles are fed into the line by a bottle unscrambler, such as our Automatic Bottle Unscramblers, which orients them upright onto the conveyor. Because dry syrup must stay dry, bottles are usually cleaned with air rather than water. An Automatic Bottle Air Jet and Vacuum Cleaning Machine blows ionised or filtered air into each inverted bottle and extracts loose particles by vacuum.
Step 2: Bottle infeed and indexing
Clean bottles arrive at the filler. The infeed worm spaces them, and a star wheel or indexing table moves each bottle into position under the filling funnel. On rotary machines, the star wheel indexes: it moves one pitch, stops while the bottle is filled, then moves again.
A sensor confirms that a bottle is present before each fill. If there is no bottle, the auger does not rotate, preventing powder from being spilled on the machine.
Step 3: Powder presentation
Powder is held in the hopper above the auger. The agitator turns slowly to prevent bridging and rat-holing and to keep the powder at a consistent density as it enters the auger flights. A level sensor monitors the powder height and triggers top-up when needed.
Step 4: Auger dosing
When the bottle is in place, the servo drive rotates the auger a precise number of revolutions. Each revolution pushes a defined volume of powder down the auger tube, through the funnel and into the bottle.
Because the volume per revolution is nearly constant, the fill weight is set by the number of revolutions. To increase the fill, the operator increases the revolution count; to decrease it, the count is reduced.
Step 5: Clean cut-off
When the auger stops, free-flowing granules can continue to trickle from the tube. To stop this, the auger tube may be fitted with a disc, spinner or fine screen at the outlet. Some machines also use a short reverse rotation of the auger, or a slight pause before the bottle moves, so the last powder settles into the bottle rather than onto the neck.
Step 6: Indexing out
The star wheel moves the filled bottle away and brings the next empty bottle under the funnel. The filled bottle travels on to the outfeed conveyor and the capping machine.
Step 7: Weight checking
At regular intervals, operators remove sample bottles and check the net fill weight. Many lines also use an in-line checkweigher after the filler to reject out-of-limit bottles and show trends. If weight drifts, the operator adjusts the auger revolution count.
Machine Configurations
Single head rotary dry syrup filler
One auger fills one bottle at a time on an indexing star wheel. This is the most common configuration for small and medium output. See the Automatic Rotary Dry Syrup Powder Filling Machine and the rotary dry syrup powder filling machine.
Double head fillers
Two augers fill two bottles at the same time, or share one larger fill between two stations, to increase output. See the auger type powder filling machine (single and double head).
Linear auger fillers
Bottles move along a straight conveyor and stop under the auger for filling. These are flexible and easy to integrate. See the Automatic Auger Type Powder Filling Machine.
Complete dry syrup lines
For full automation, the filler is combined with bottle handling, capping and sealing into one synchronised line. See the automatic dry syrup powder filling line.
Browse all powder filling machines, the dry syrup powder filling machines range and our dry powder filling machines.
How Fill Weight Is Controlled
Fill weight in an auger filler depends on two things: the volume delivered and the bulk density of the powder at the moment of filling. The main controls are:
| Control | Effect |
|---|---|
| Auger revolutions | Main fill weight adjustment |
| Auger and tube size | Chosen to match the fill weight; affects resolution and speed |
| Agitator speed | Keeps density even; too fast can aerate, too slow allows bridging |
| Hopper level | A steady level gives steady density at the auger inlet |
| Auger speed and acceleration | Affects how cleanly powder is delivered |
| Cut-off device | Prevents dribble after the auger stops |
Choosing the right auger
Auger tooling is one of the most important decisions when setting up a dry syrup filler. An auger that is too large for the fill weight needs very few revolutions, so small adjustments cause large changes. An auger that is too small needs many revolutions, slowing the machine. Suppliers usually recommend tooling after testing samples of the actual powder.
Humidity, Temperature and Product Protection
Many dry syrup powders are hygroscopic: they absorb moisture from the air. Moisture causes caking, poor flow, density changes and, in some cases, loss of product stability. That is why dry syrup filling is usually carried out in a room with controlled relative humidity and temperature.
Good practice includes:
- Keeping the hopper covered and filling it from closed containers
- Limiting how long powder is exposed in the hopper
- Filling and capping bottles promptly after filling
- Using induction sealing to provide a moisture barrier and tamper evidence
- Monitoring room conditions throughout the batch
The required conditions depend on the specific product, so always refer to the product’s development data and your own quality procedures.
Dust Control and Cross-Contamination
Dry syrups often contain antibiotics, so dust control is important for operator safety and to prevent cross-contamination between products. Machines limit dust by:
- Placing the funnel close to or inside the bottle mouth
- Fitting dust extraction at the filling point
- Using enclosed hoppers and closed transfer systems
- Choosing smooth, polished contact parts that are easy to clean
Dedicated facilities or strict cleaning and changeover procedures are commonly used for certain antibiotic classes. Always confirm requirements against current applicable regulatory guidelines.
The Complete Dry Syrup Line
A typical line looks like this:
- Bottle unscrambler – orients and feeds bottles
- Air jet and vacuum cleaning – cleans bottles without water
- Dry syrup powder filling – auger dosing
- Capping – ROPP or screw capping, for example on a bottle screw and ROPP capping machine. For the ROPP process, read our bottle ROPP capping machine working principle. See also the capping machines for glass and PET bottles.
- Induction sealing – seals a foil liner to the bottle lip, using an induction sealing machine
- Labelling – on a bottle sticker labeling machine; the label often carries the reconstitution mark and instructions
- Cartoning – often with a measuring cup or dosing device and a leaflet
Line speeds should be balanced so the filler, capper and sealer work together without bottles waiting with open necks.
Troubleshooting Common Dry Syrup Filling Problems
| Problem | Likely Cause | Corrective Action |
|---|---|---|
| Fill weight drifting | Falling hopper level, changing density, rising humidity | Control level, check room conditions, adjust revolutions |
| Random light fills | Bridging in the hopper | Adjust agitator, check powder condition |
| Powder dribbling after fill | Free-flowing granules | Fit a cut-off disc or screen, add reverse rotation |
| Powder on bottle neck | Funnel misaligned, bottle moved too early | Align funnel, add settling pause |
| Excess dust | Funnel too high, weak extraction | Lower funnel, improve extraction |
| Caking in hopper | High humidity, long exposure | Improve humidity control, reduce hopper time |
| Bottles jamming | Wrong change parts, worn star wheel | Fit correct parts, replace worn items |
| Leaking or loose caps downstream | Powder on bottle neck preventing seal | Improve filling cleanliness |
Maintenance Tips
- Inspect the auger and tube for wear and scratches; a worn auger changes volume per revolution.
- Clean the hopper, agitator, auger and funnel thoroughly between batches and products.
- Check that the agitator and auger drives run smoothly.
- Verify level sensors and “no bottle, no fill” sensors regularly.
- Keep change parts and auger tooling labelled for each bottle size and product.
- Trend fill weights to catch gradual changes early.
Changeover Between Products and Bottle Sizes
- Empty the hopper and remove product contact parts
- Clean according to the validated procedure
- Fit the auger and tube tooling for the new fill weight
- Change the star wheel, worm and guides for the new bottle
- Set the auger revolution count and machine speed
- Run trial bottles and confirm fill weight before production
How to Choose a Dry Syrup Filling Machine
- Fill weight range and the auger tooling required
- Powder properties – flowability, density and hygroscopicity
- Required output – single or double head, standalone or full line
- Bottle sizes and materials
- Dust control and cleanability
- Integration with capping, induction sealing and labelling
- GMP documentation and qualification support
Frequently Asked Questions
What is the working principle of a dry syrup filling machine? An auger rotates a set number of revolutions to deliver a measured volume of powder into each bottle, while a star wheel indexes bottles under the filling head.
How is fill weight adjusted? Mainly by changing the number of auger revolutions, with tooling selected to suit the fill range.
Why is humidity control important? Many dry syrup powders absorb moisture, which causes caking, poor flow and density changes that affect fill accuracy and product quality.
Why are bottles cleaned with air instead of water? Any moisture left in the bottle could affect the powder. Air jet and vacuum cleaning removes particles without wetting the bottle.
Why is induction sealing used on dry syrup bottles? It adds a moisture barrier and tamper evidence under the cap.
Planning a dry syrup filling line? Contact our team or send an inquiry with your powder details, fill weights and bottle sizes.