
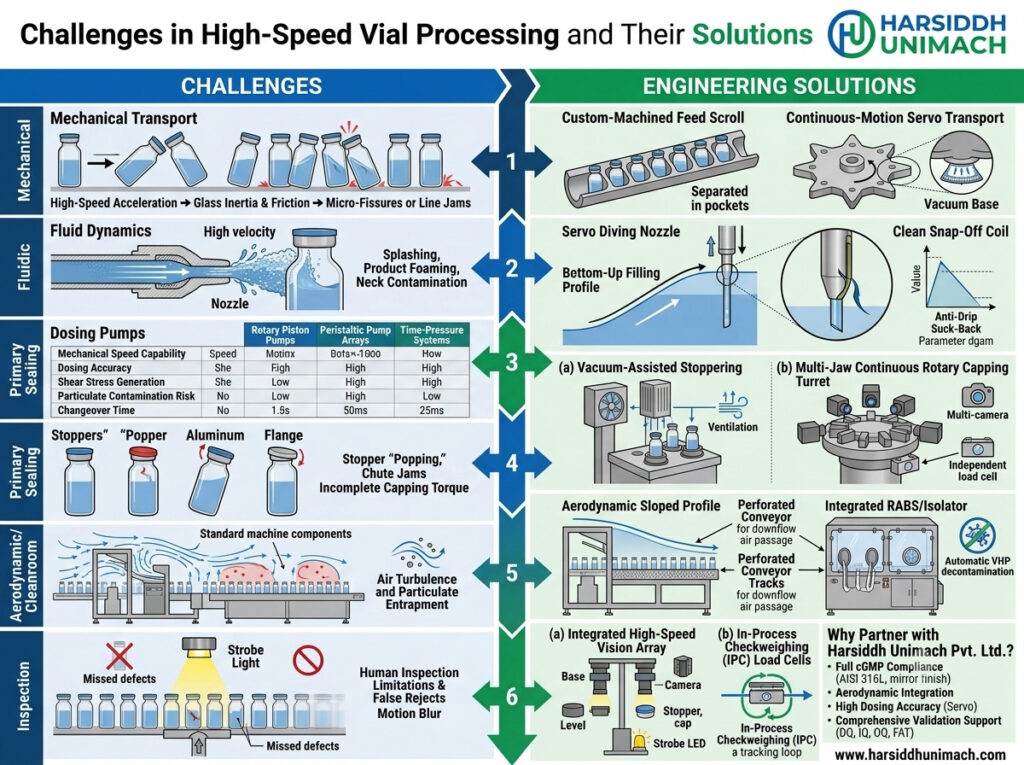
As demand for injectable medicines grows, manufacturers are under pressure to produce more vials, faster, without compromising quality or sterility. High-speed vial lines make this possible — but speed brings its own set of challenges. Every weakness in container quality, machine setup, line balance or operator practice is amplified when hundreds of vials pass through each station every minute.
A line that runs well at moderate speed may suffer breakage, fill weight drift, stopper problems and frequent stoppages when pushed harder. The result is lower real output, more rejects and more interventions in the critical zone — the opposite of what the investment was meant to achieve.
In this guide, we look at the most common challenges in high-speed vial processing, explain what causes them and share practical solutions that help lines run fast, clean and consistently.
Why Speed Changes Everything
At higher speeds:
- Forces increase: acceleration, deceleration and transfer impacts are greater, so glass is under more stress.
- Time windows shrink: filling, stoppering and crimping must be completed in fractions of a second.
- Small errors multiply: a minor misalignment that causes one problem an hour at low speed may cause dozens at high speed.
- Stoppages cost more: every minute of downtime represents a larger number of lost vials.
- Interventions rise: jams and faults draw operators into the Grade A zone more often, increasing contamination risk.
Understanding these effects is the first step to designing and running a reliable high-speed line.
Challenge 1: Vial Breakage and Glass Handling
The problem
Broken and chipped vials stop the line, create glass particles and require line clearance — sometimes leading to rejection of nearby vials. Glass fragments can also contaminate the filling zone.
Common causes
- Glass-to-glass contact on crowded conveyors and turntables
- Misaligned star wheels, guides and infeed worms
- Incorrect change parts for the vial size
- Variation in vial dimensions from the supplier
- Thermal shock when vials exit the tunnel too hot
- Sudden starts and stops
Solutions
- Use servo-driven transfers with smooth acceleration profiles
- Control accumulation pressure on turntables and conveyors
- Verify vial dimensions and tolerances with suppliers
- Use clearly identified, correctly sized change parts and check alignment at every changeover
- Ensure the tunnel cooling zone delivers vials at a safe temperature
For a deeper look, read our article on the top 5 causes of vial breakage on high-speed filling lines.
Challenge 2: Maintaining Fill Accuracy at Speed
The problem
As speed increases, the time available to dose each vial decreases. Pumps must deliver the same volume faster, which can lead to fill weight variation.
Common causes
- Air entrapment in the product line
- Pump wear, especially seals and valves
- Product viscosity changes with temperature
- Pressure fluctuations in the product supply
- Mechanical lag in cam-driven systems
Solutions
- Use servo-driven dosing with programmable fill profiles
- Keep product supply pressure and level stable with a buffer vessel
- Control product temperature
- Perform regular in-process fill weight checks and trend the results
- Replace wear parts on a preventive schedule
Servo technology is especially valuable at high speed. Learn why in how servo-driven vial filling systems outperform mechanical lines.
Challenge 3: Foaming, Splashing and Wet Necks
The problem
Fast filling increases turbulence. Product can foam, splash onto the vial neck or stopper seating area, and even overflow.
Common causes
- Nozzles filling from the top instead of diving
- Fill speed too high for the product
- Incorrect nozzle diameter
- Poor drip control at the end of the dose
Solutions
- Use diving nozzles that fill from the bottom up and rise with the liquid level
- Program slow-fast-slow fill profiles
- Select nozzle sizes to suit product viscosity and fill volume
- Set suck-back correctly to prevent drips
Challenge 4: Stopper Feeding and Seating
The problem
At high speed, stopper bowls and chutes must deliver a continuous supply of correctly oriented stoppers. Jams, missing stoppers and raised or tilted stoppers are common causes of stoppages and interventions.
Common causes
- Stopper bowls not tuned for the stopper type
- Stoppers sticking together due to siliconisation level or static
- Worn pick-up heads or stoppering wheels
- Misalignment between vial and stopper at the placement point
Solutions
- Tune vibratory bowls and chutes for each stopper type
- Work with stopper suppliers on consistent dimensions and surface treatment
- Use reliable stopper presence and height detection with automatic rejection
- Maintain stoppering heads and check alignment at every changeover
A robust filling and stoppering machine, such as our liquid vial filling machine with rubber stoppering or the Automatic Rotary Vial Filling Machine, is designed to keep stopper placement precise at speed.
Challenge 5: Crimping Quality and Container Closure Integrity
The problem
High-speed capping must apply aluminium seals consistently to every vial. Loose seals threaten container closure integrity, while excessive force cracks vial necks.
Common causes
- Incorrect crimping roller pressure or position
- Variation in vial neck or seal dimensions
- Worn rollers or heads
- Insufficient capping capacity, forcing heads to run too fast
Solutions
- Use multi-head capping machines sized for the line output, such as the Automatic Eight Head Vial Cap Sealing Machine or our 1, 4, 6 and 8 head vial cap sealing machines
- Set and verify crimping parameters for each vial and seal combination
- Inspect seals regularly and maintain rollers
Challenge 6: Line Balancing and Micro-Stops
The problem
A high-speed line is only as fast as its slowest station. If the washer, tunnel, filler, capper, inspection and labelling machines are not balanced, vials back up, machines stop and restart, and output falls far below rated speed. Short “micro-stops” of a few seconds can add up to significant lost time.
Common causes
- Downstream machines rated at the same speed as the filler, leaving no recovery margin
- Insufficient accumulation between machines
- Poor communication between machine controls
- Upstream stations, such as the washer or tunnel, limiting supply
Solutions
- Treat the filler as the key machine and rate upstream and downstream equipment slightly faster
- Add accumulation tables at critical points, such as after the tunnel and before labelling
- Synchronise machine controls so speeds adjust automatically
- Ensure upstream equipment — such as the linear vial washing machine and sterilizing tunnel for ampoules and vials — has sufficient capacity
Challenge 7: Changeovers and Format Flexibility
The problem
High-speed lines are often expected to run several products and vial sizes. Long changeovers erode the productivity gains of speed.
Common causes
- Many loose change parts requiring tools
- Manual adjustments that rely on operator experience
- No stored settings for each format
- Cleaning and sterilisation of product-contact parts taking too long
Solutions
- Use tool-less, colour-coded change parts
- Store recipes for each product and vial size
- Use quick-release product-contact parts and single-use product paths where suitable
- Standardise changeover procedures and train teams
Read more in our article on running multiple vial sizes on a single line.
Challenge 8: Sterility Assurance and Interventions
The problem
Every jam, fallen vial or stopper problem at high speed can require an operator to intervene in the Grade A zone. Frequent interventions increase contamination risk and are closely scrutinised by regulators.
Solutions
- Reduce the root causes of jams — breakage, stopper feed problems and misalignment
- Design machines with barrier technology and glove ports for safe interventions
- Define and qualify each type of intervention
- Track interventions per batch as a key quality indicator
Challenge 9: Product Loss
The problem
High-speed lines can lose significant product during start-up, at changeovers, through rejected vials and in the hold-up volume of tubing and pumps. For high-value products, this is a major cost.
Solutions
- Minimise product path volume
- Use recovery procedures at the end of each batch
- Reduce start-up rejects by stabilising machine settings quickly
- Use no-vial-no-fill logic to prevent dosing into empty positions
Our guide on how to minimise product loss during high-speed production explores these strategies in detail.
Challenge 10: Inspection and Labelling Keeping Pace
The problem
Downstream stations must handle every vial produced. If inspection or labelling cannot keep up, they become bottlenecks — or quality is compromised.
Solutions
- Use inspection systems sized for line output, such as our visual ampoule and vial inspection machine, and consider automation for high volumes
- Clean and dry vials before labelling with an automatic external vial washing machine
- Use precise, high-speed labellers such as our vertical vial sticker labeller
Challenge 11: Wear and Maintenance at High Cycle Rates
The problem
Machines running at high speed accumulate cycles quickly. Seals, bearings, grippers, rollers and sensors wear faster, and gradual wear shows up as fill drift, misalignment and breakdowns.
Solutions
- Base maintenance on running hours or cycles, not just calendar time
- Monitor trends such as fill weight variation and reject rates as early warnings
- Keep critical spare parts in stock to avoid long waits
See our 7 best practices to prevent unscheduled downtime and the list of essential vial filling machine spare parts to keep in stock.
Challenge 12: Operator Skills and Data
The problem
High-speed lines are more complex to operate and troubleshoot. Without skilled operators and good data, problems are fixed temporarily rather than permanently.
Solutions
- Train operators on setup, troubleshooting and the reasons behind each setting
- Use HMI alarm histories and production data to identify recurring problems
- Hold regular reviews of downtime causes and reject trends
- Involve operators in improvement projects
Measuring Success: OEE
Overall Equipment Effectiveness (OEE) is a useful way to measure how well a high-speed line performs. It combines:
- Availability – how much of the planned time the line actually runs
- Performance – how fast it runs compared with its rated speed
- Quality – how many good vials are produced compared with the total
Each challenge above affects one or more of these factors. Tracking OEE and its components helps you focus improvement efforts where they will have the greatest impact.
Summary: Challenges and Solutions at a Glance
| Challenge | Key Solution |
|---|---|
| Vial breakage | Smooth servo transfers, correct change parts, controlled accumulation |
| Fill accuracy | Servo dosing, stable supply, temperature control |
| Foaming and wet necks | Diving nozzles, fill profiles, suck-back |
| Stopper problems | Tuned feeders, quality stoppers, reliable detection |
| Crimping quality | Correctly sized multi-head cappers, verified settings |
| Line imbalance | Rated margins, accumulation, synchronised controls |
| Slow changeovers | Tool-less parts, recipes, standard procedures |
| Interventions | Root-cause fixes, barrier technology |
| Product loss | Minimal hold-up, recovery, stable start-up |
| Downstream bottlenecks | Adequately sized inspection and labelling |
| Wear | Cycle-based maintenance, spares |
| Skills and data | Training, alarm analysis, continuous improvement |
Frequently Asked Questions
What is the most common problem in high-speed vial processing? Vial breakage and line stoppages caused by handling issues and poor line balance are among the most common and costly problems.
How can fill accuracy be maintained at high speed? By using servo-driven dosing, stable product supply, temperature control and regular in-process weight checks.
Why do stoppers cause so many stoppages? Stopper feeding is sensitive to stopper dimensions, surface treatment and bowl tuning. Small variations cause jams or misplacement at high speed.
What is line balancing? Matching the capacity of each station so the filler can run steadily, with slightly faster upstream and downstream machines and accumulation between them.
How do high-speed lines affect sterility? More jams and faults can increase interventions in the Grade A zone. Reducing root causes and using barrier technology protects sterility.
Planning or improving a high-speed vial line? Explore our vial filling machines, the vial filling machines for liquid vials and our vial washing machines, contact our team or send an inquiry.